fabricación de pinturas y tintas

Introduction

Oliver & Batlle began using vacuum loading systems in complex industrial applications many years ago. The experience gained with difficult-to-handle powdered products such as Aerosil, carbon black, glass microspheres and bentonite prompted O+B to develop an R&D project focused on creating a specific solution for this application: the vacuum loading system for powdered raw materials, called DISPERVAC.

DISPERVAC solves the problem of loading raw materials that are difficult to handle due to their volatility, dirtiness, contaminating characteristics or health risks.

Several chemical industry machinery manufacturers have been introducing inline mixing systems to the market for years for the incorporation of powdered raw materials into dispersion processes. With the aim of offering a robust and competitive alternative, Oliver & Batlle developed the DISPERVAC system, which combines vacuum feeding of solids with the Polimix dispersion system, achieving a highly efficient, safe, and versatile solution. After analysing the various processes available on the market, we believe our DISPERVAC technology is also particularly interesting for incorporating pigments such as titanium dioxide (TiO?), which is widely used in the paint industry for its hiding power and colorimetric performance but is difficult to handle and expensive.

In the next article, we will present some ideas that will support the promotion and use of the DISPERVAC system, which we hope will be of interest to you.

Advantages of vacuum loading of powdered products with the DISPERVAC system in paint and ink manufacturing

Nowadays, pigment cost is one of the most significant factors in the manufacturing of paints and inks. Reducing pigment usage can represent a considerable cost savings and improve overall process profitability.

One of the most widely used pigments is titanium dioxide (TiO?) a costly and difficult-to-handle material. Depending on the formulation, it can suppose for 25% to 40% of the total production cost. There has long been ongoing discussion around the possibility of classifying TiO? as a carcinogenic substance, which could eventually lead to regulations restricting its use.

In anticipation of such a scenario, Oliver + Batlle has developed a vacuum powder loading system compatible with dispersion machines, designed to streamline the handling of powdered pigments and facilitate their safe and efficient incorporation into the production process.

Vacuum loading of powdered pigments in paint and ink manufacturing offers major advantages, especially for dispersing pigments such as TiO?:

  1. Enhances the colorimetric strength of the pigments.
  2. Allows for reduced pigment usage, as air-free dispersions ensure better particle distribution and more efficient processing, avoiding the “airbag effect” caused by excess air.

DISPERVAC: An ultra-efficient vacuum dispersion method

The DISPERVAC system consists of two main units:

  • A powder handling and transfer system, equipped with vacuum technology. 
  • A production unit based on coaxial conical dispersion technology, specifically designed to operate under vacuum conditions. 

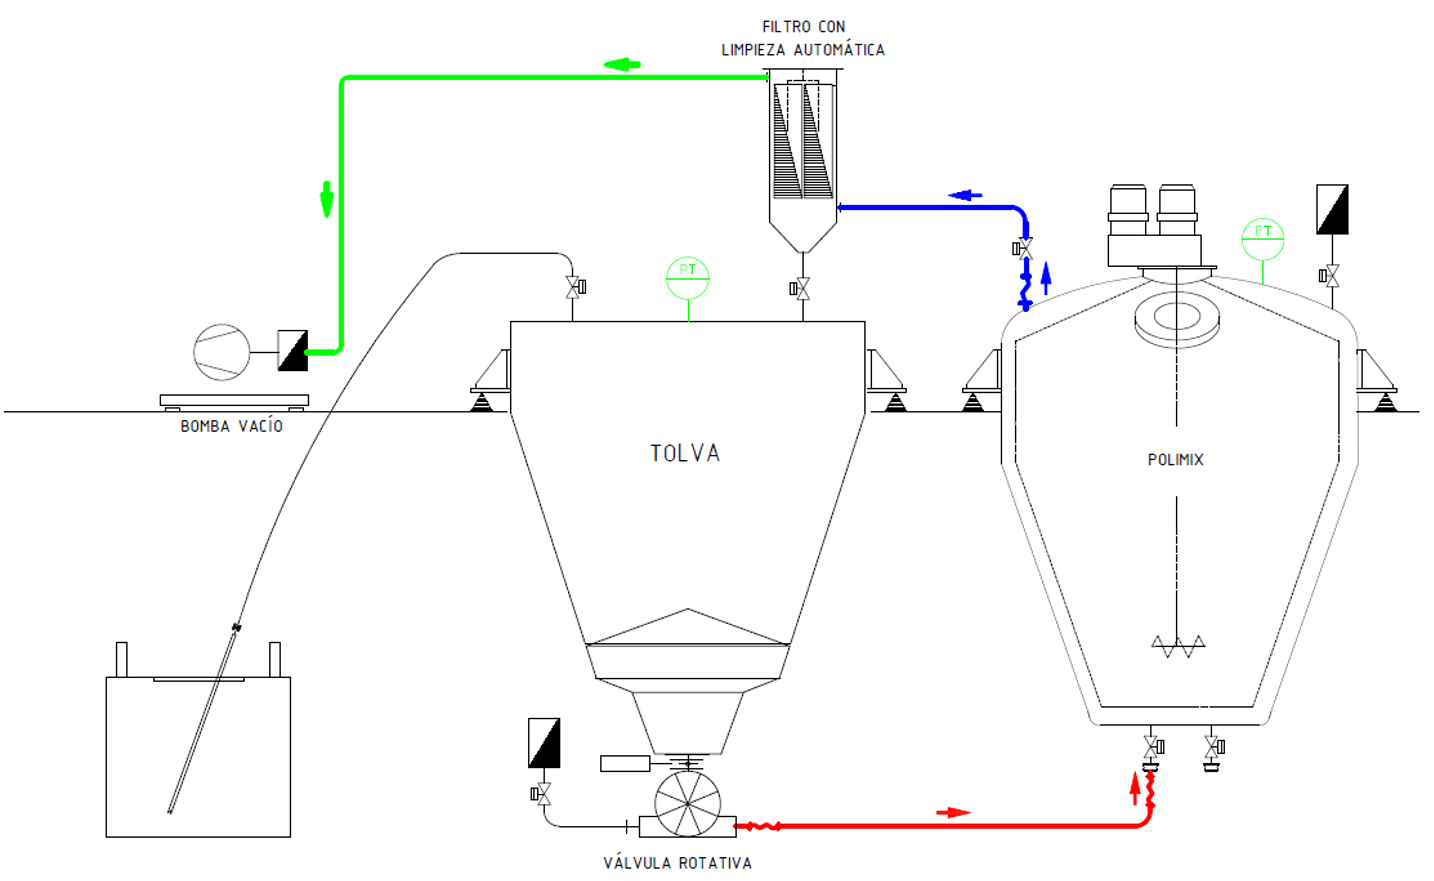
The vacuum handling system is particularly suitable for highly volatile or fine powders, such as aluminum silicates or glass microspheres, as well as for various pigments and fillers like TiO?, calcium carbonate, talc, or silica. Oliver + Batlle offers the system in two configurations:

  • With a sealed vessel where the full powder formula can be prepared, as shown in the diagram:
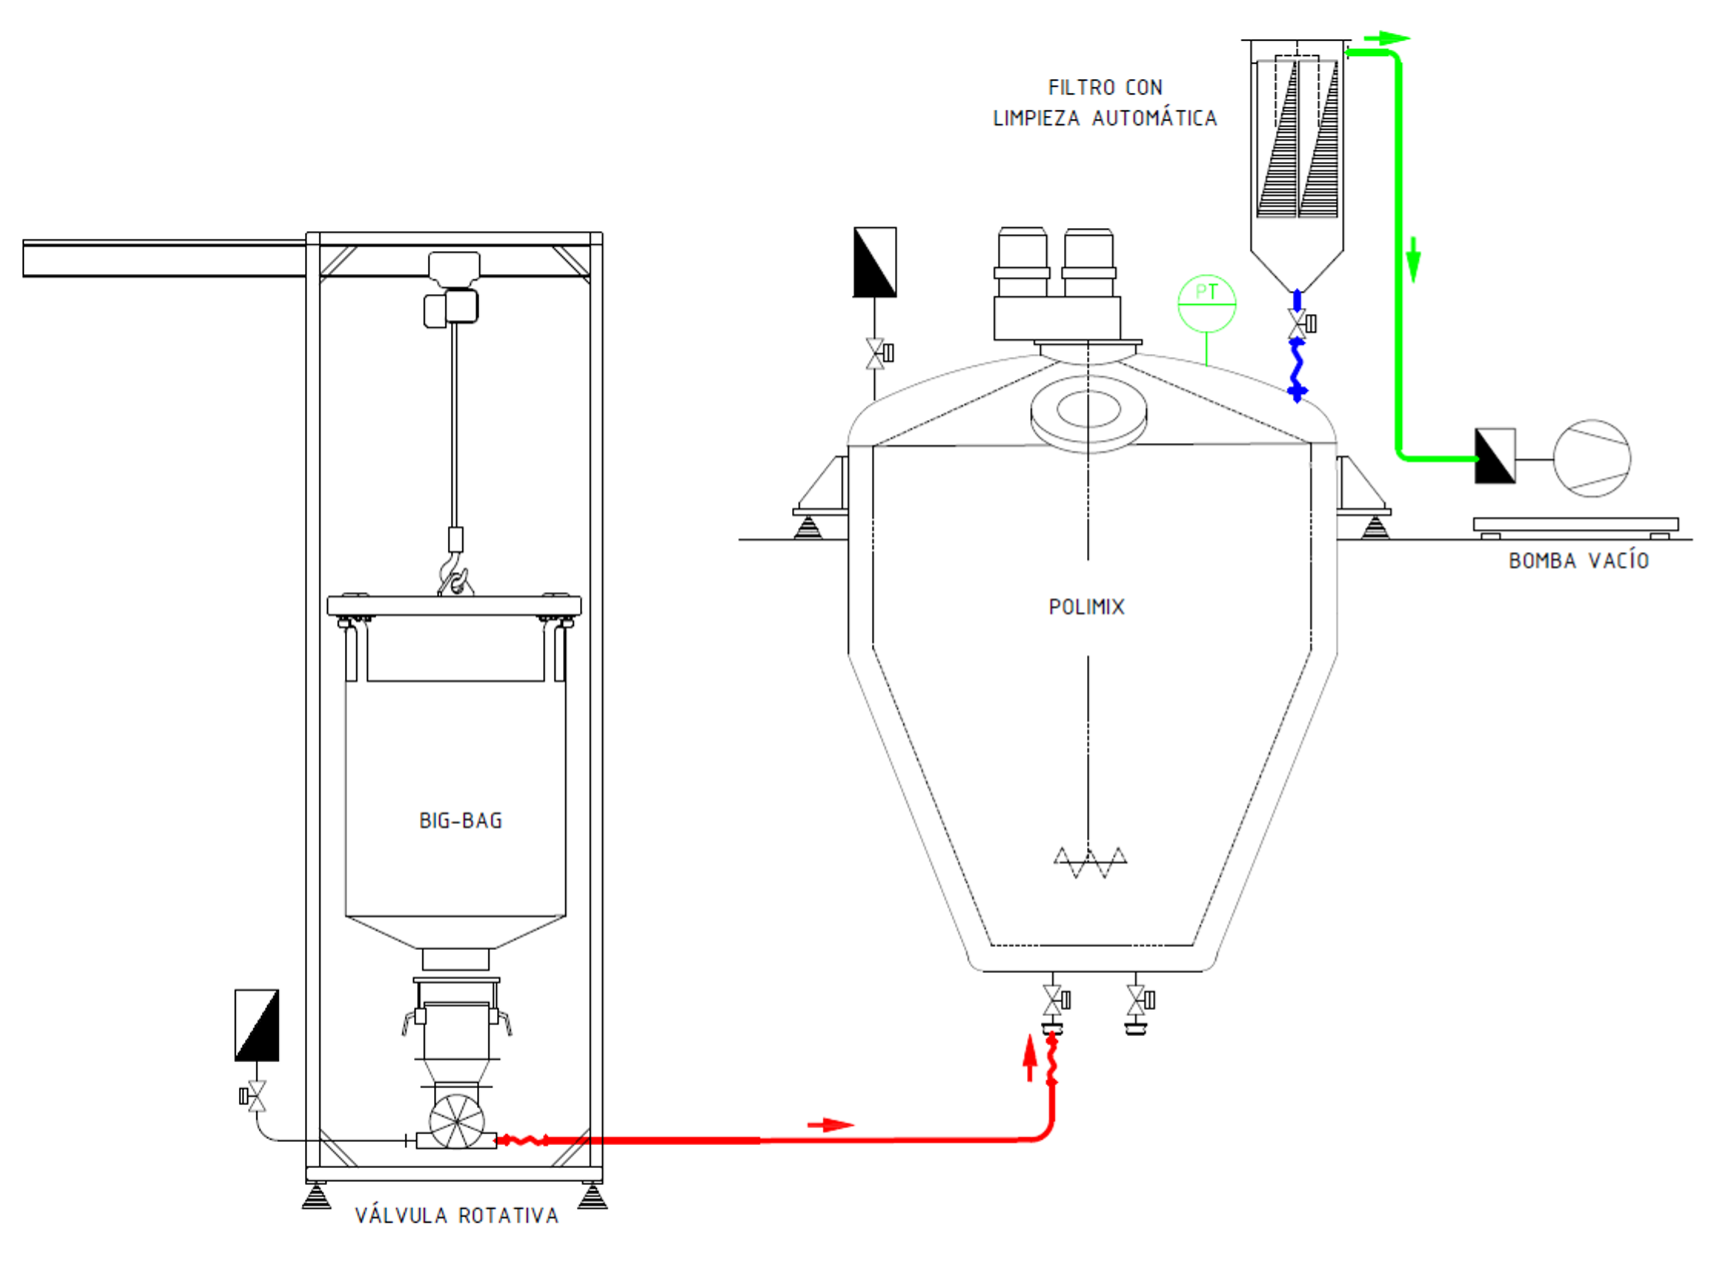
  • With solutions adapted to powders supplied in big bags or standard 25 kg sacks.
 

In the first case, the preload hopper can be used to prepare the powder mix before transferring it to the manufacturing unit.

The vacuum system is used for two main operations:

  1. Powder raw material loading 
  2. Air extraction from the finished product 

DISPERVAC can be fully parameterized for each product, allowing a wide range of powders to be handled regardless of their bulk density or particle size.

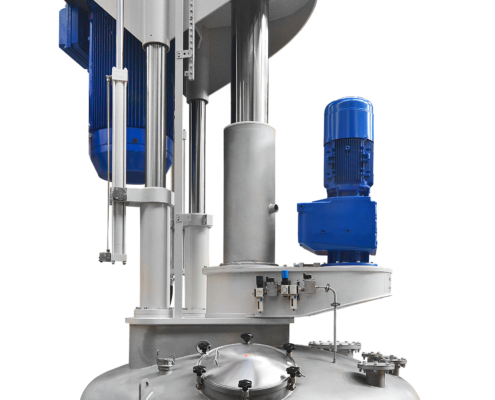
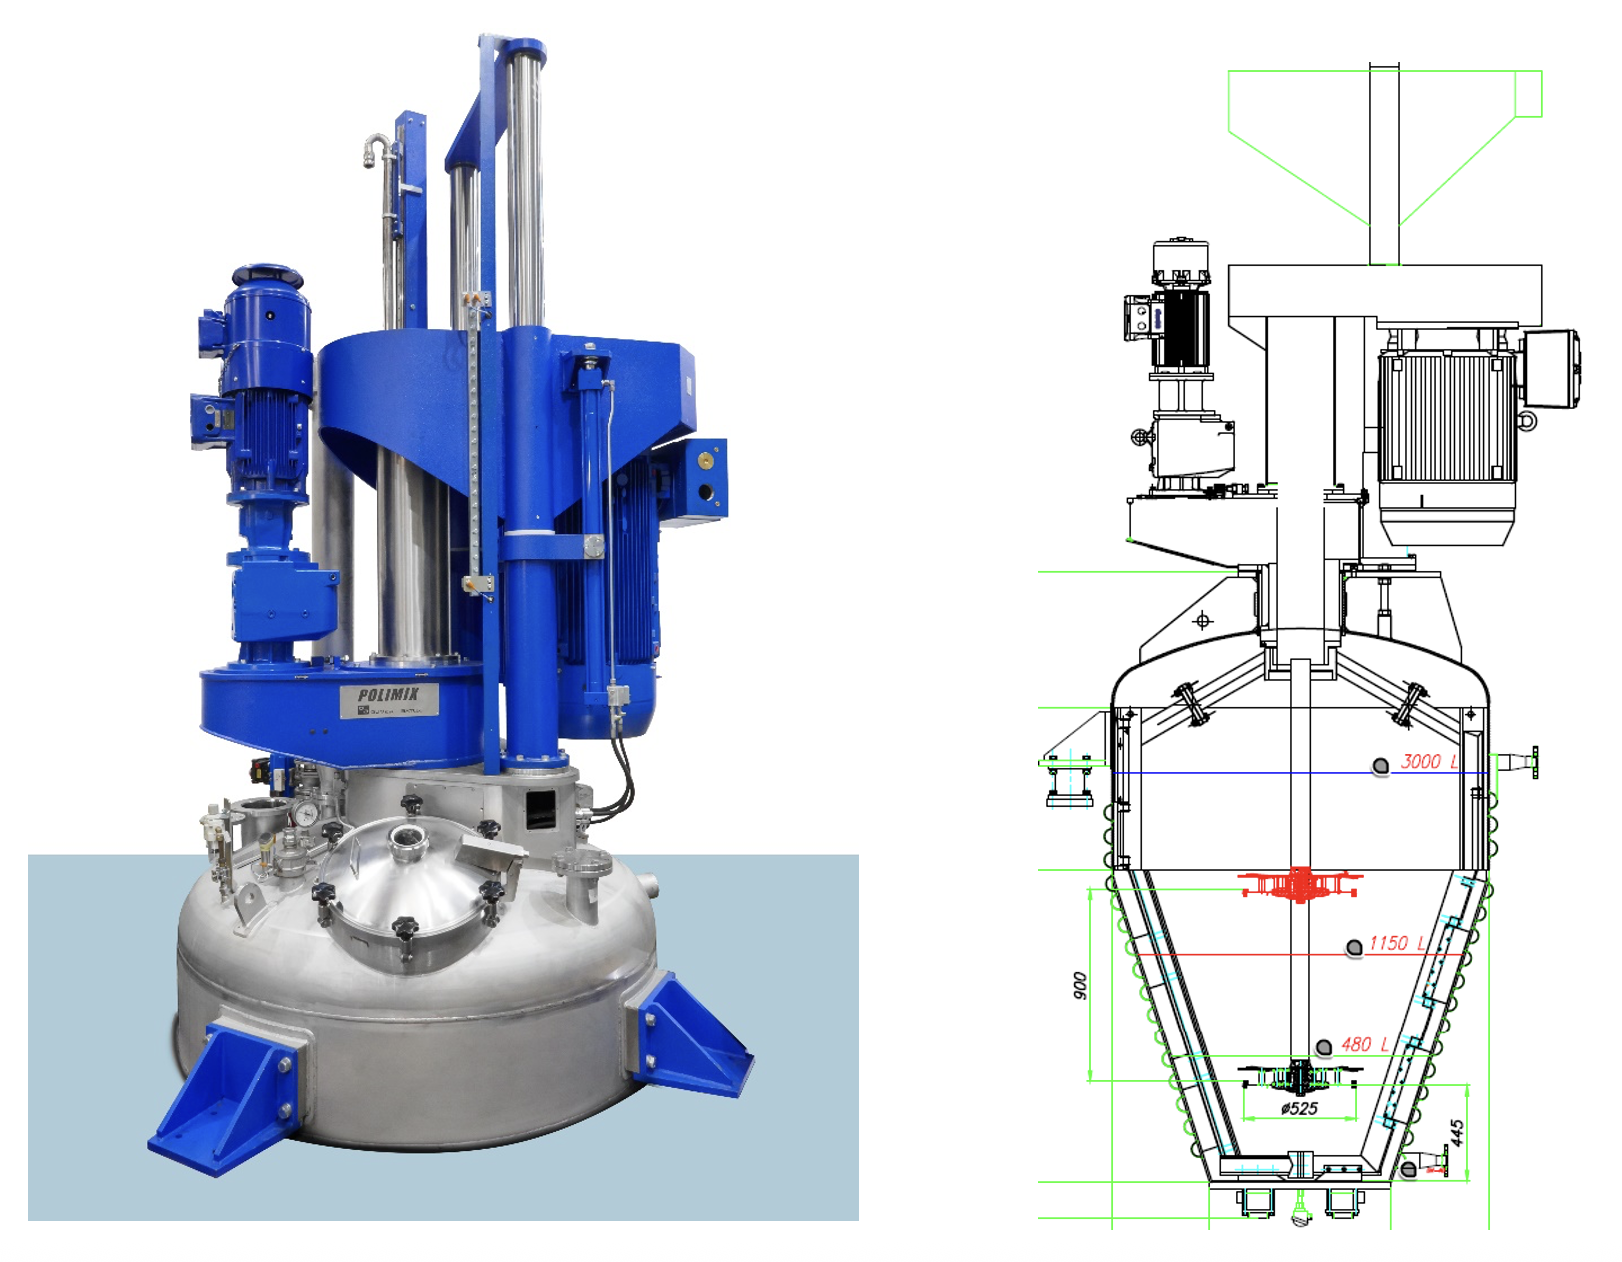
The production unit must be airtight and designed for vacuum operation. For maximum dispersion efficiency, we recommend using a Polimix vessel of conical trunk form equipped with two coaxial agitation systems:

  • A dispersing unit with one or two turbines featuring lift/lower mechanisms. 
  • An anchor-type homogenizer with flexible wall scrapers to ensure optimal mixing. 

These machines are highly efficient in dispersion processes, since vacuum loading takes place from the bottom of the vessel, enabling immediate incorporation of pigments into the liquid flow generated by the dispersion turbine. This avoids pigment floating or surface accumulation, which is common in top-loading systems.

The conical shape conduces the powders directly into the primary turbine, allowing the process to begin with a minimal amount of liquid. When using an appropriate dispersant—in both type and quality—excellent dispersion results are achieved.

The DISPERVAC system allows the handling of powdered products by vacuum, completely avoiding dust emissions during loading and associated material losses. It is particularly suitable for low-density products or those requiring special handling conditions due to health hazards for plant operators—such as TiO?.

The vacuum suction system can be fully programmed, allowing pigments to be introduced into the formulation at a controlled and repeatable feed rate.

The adition of pigments in paint and ink manufacturing is a critical and sometimes complex operation. With the programmable DISPERVAC system, a precise and repeatable process is guaranteed, enabling the optimal incorporation of pigments free from entrapped air. This air-free dispersion improves pigment performance, increases color strength, and reduces raw material costs in formulations.


What kind of manufacturing equipment is used in a DISPERVAC installation? 

Using dispersers equipped with saw-tooth turbines or HDM-type turbines, as traditionally done, remains an effective method—especially when operating with tanks whose geometry enhances turbine efficiency, such as trunk conical shapes.

This geometry allows the dispersion phase to begin with minimal liquid volume, increasing the effectiveness of the turbines. In large-capacity machines, a small turbine can be placed at the bottom and a second, larger one in an intermediate position. Even when both turbines operate simultaneously, the required installed power does not need to be high.


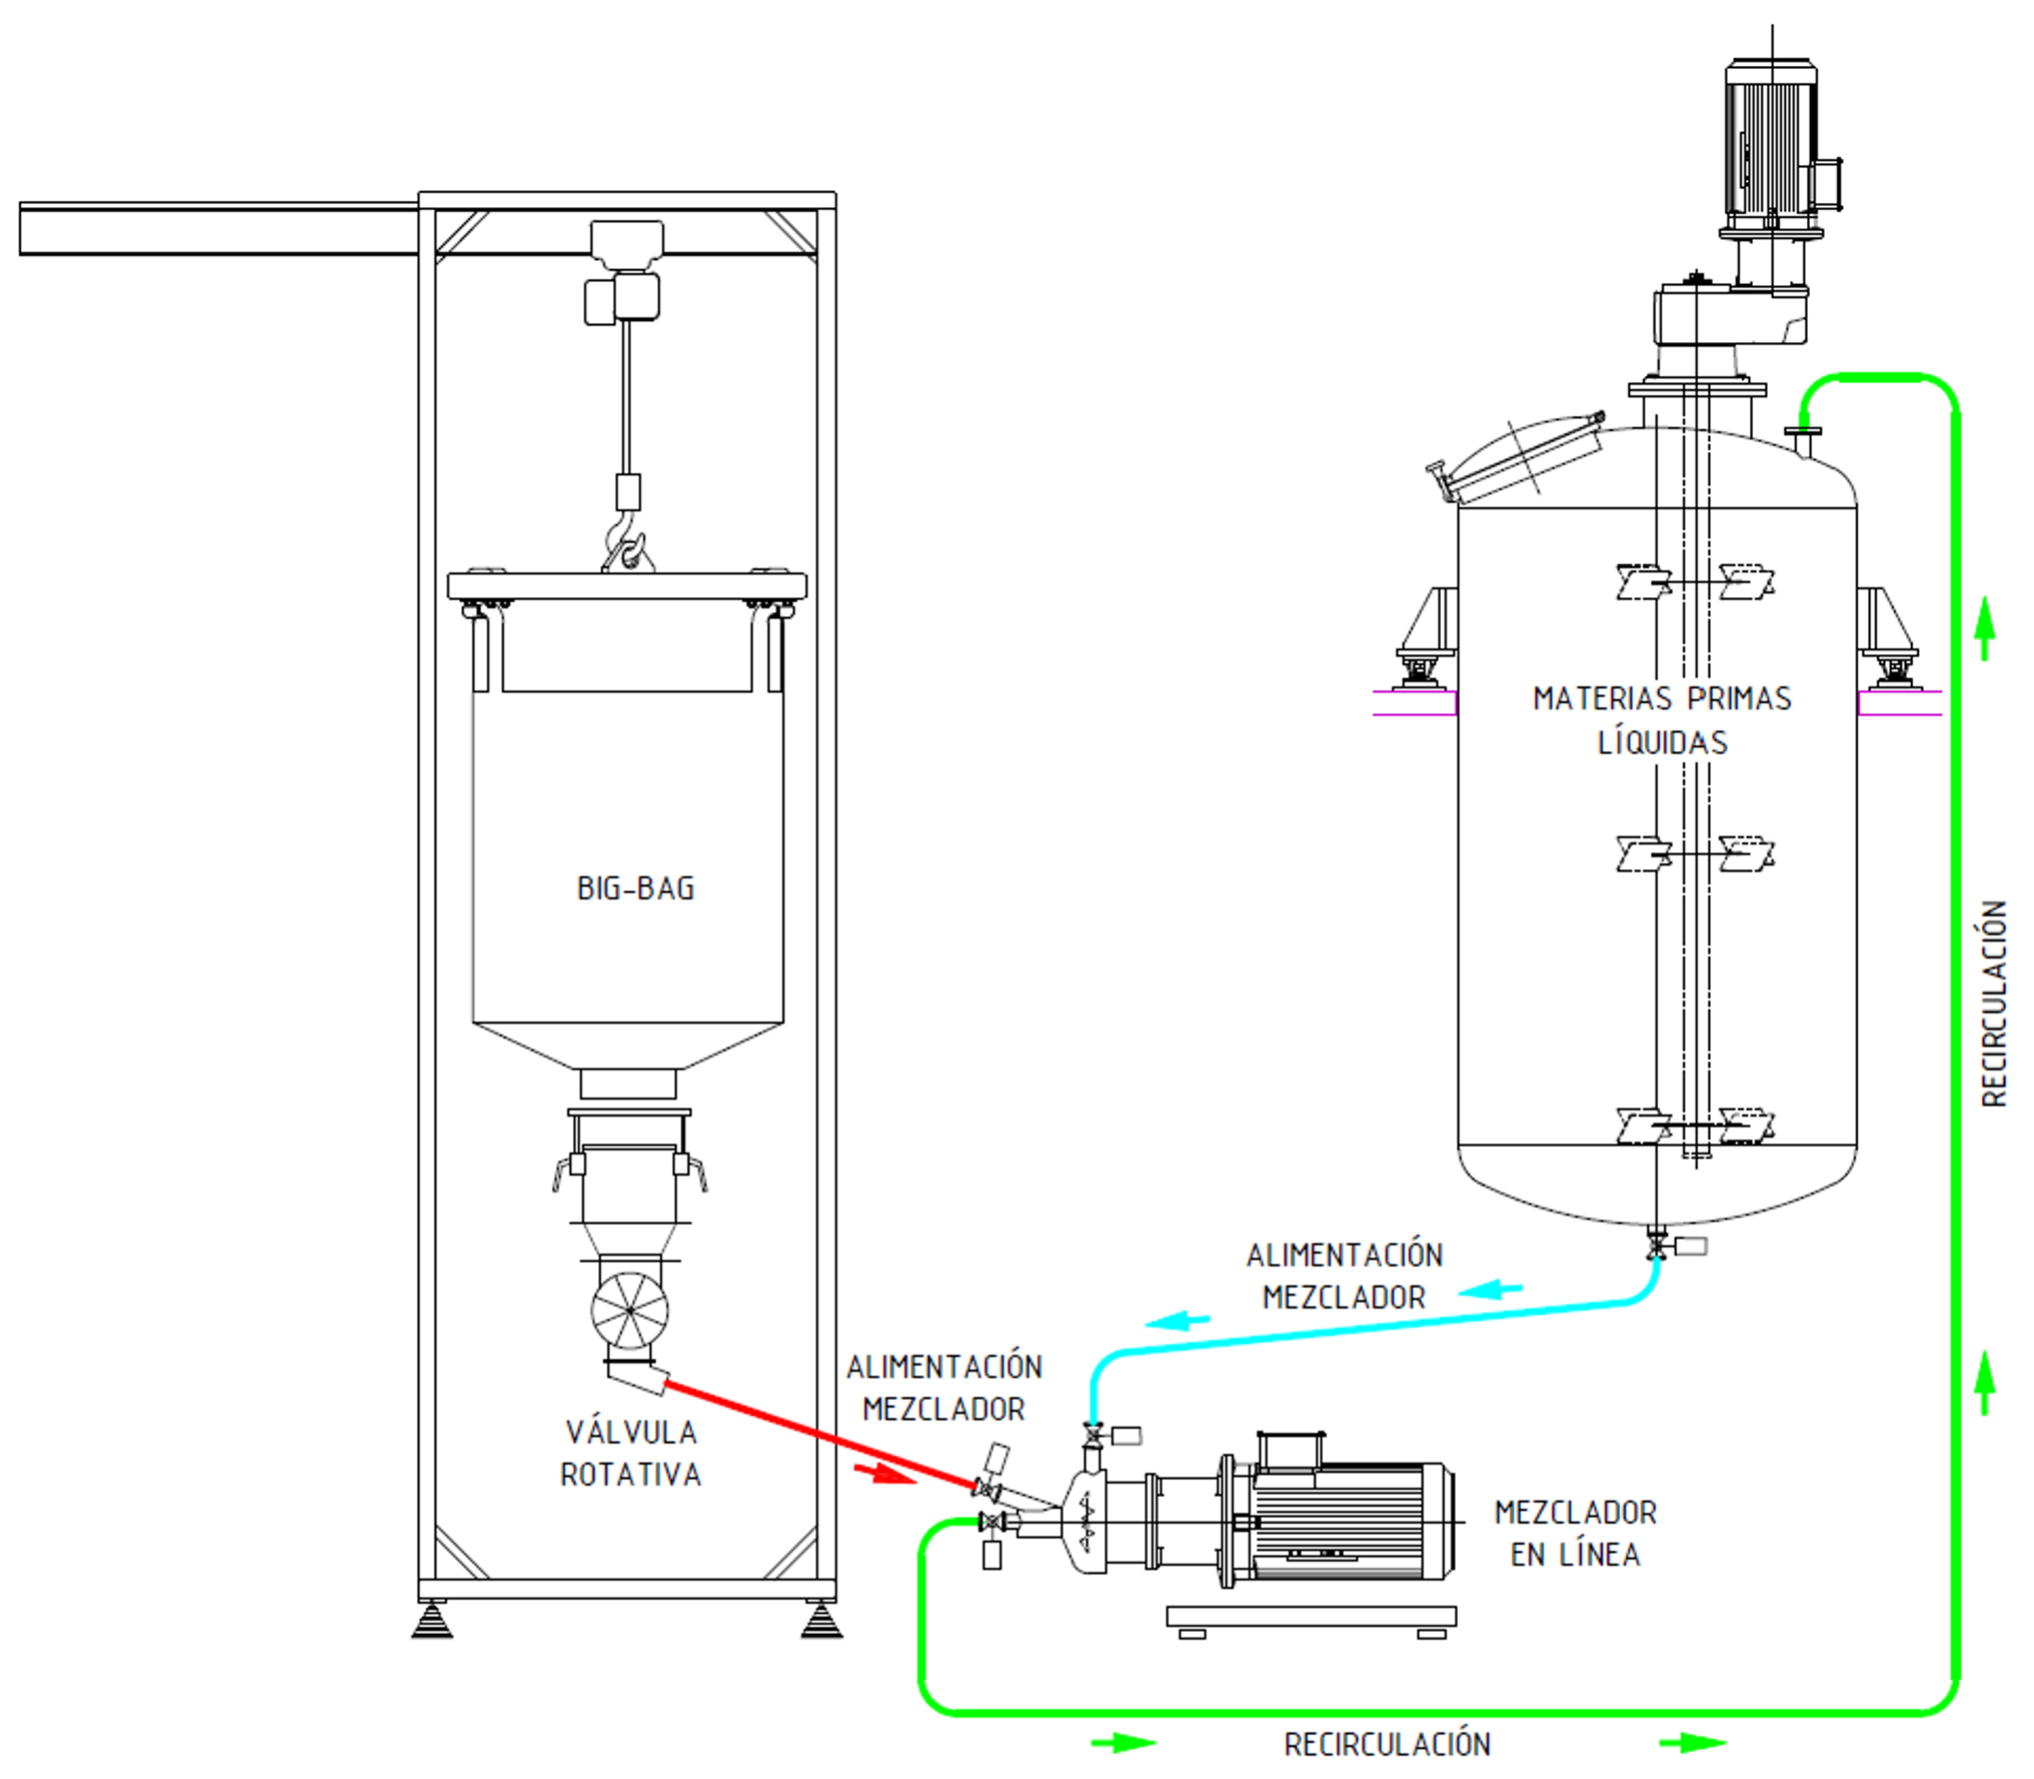
Comparing the DISPERVAC system with inline mixing processes

Inline vacuum dispersion systems promoted in the market often claim the advantage of lower installed power. However, this argument must be linked to the speed of the dispersion process.

To achieve faster dispersion times than a traditional disperser—and to ensure sufficient suction capacity for powdered pigments—inline mixers must operate at very high speeds, which in turn requires high power consumption (according to available technical data, some machines reach up to 110?kW).

Additionally, inline mixers require a recirculation and homogenization tank, which also needs to be equipped with an agitator. The required power for this agitator depends on the batch volume. In total, the combined power requirement of an inline system often exceeds that of a Polimix coaxial trunk conical disperser.

Another often-overlooked challenge in inline dispersion systems is the temperature rise within the dispersion chamber. This can be particularly problematic for solvent-based formulations containing volatile or flammable components.

Moreover, air removal from powder-based raw materials during the inline dispersion process is only possible if a dedicated vacuum system is installed—something that is frequently not included in standard configurations.
Air removal during the DISPERVAC manufacturing process

Many pigments used in the production of paints and inks contain entrapped air, which can account for 25% to 30% of their volume. When vacuum loading is applied, a small amount of air is introduced to help transport the powder into the disperser.

Additionally, saw-tooth turbine dispersers tend to incorporate small amounts of air during the shearing process. While the presence of air at certain points during pigment dispersion can aid in wetting the pigment particle surfaces, it can become problematic later in the process.

Excess air at the end of production may lead to volume instability or air bubbles appearing during application. With the DISPERVAC system, these issues are eliminated, as the same vacuum system used for loading can also extract residual air from the final product.

An air-free production process ensures a more uniform particle distribution and prevents foaming or bubble formation during paint or ink application. In printing inks, the removal of air enhances gloss and visual performance.

Foam caused by air entrapment in conventional dispersion processes is often corrected by adding defoamers. However, manufacturing with DISPERVAC allows for vacuum-based air extraction, significantly reducing—or even eliminating—the need for antifoaming agents and consequently lowering formulation costs.


Pigment and filler incorporation with the DISPERVAC system

In a traditional water-based decorative paint manufacturing process using cylindrical tanks, the dispersion of TiO? usually starts with the maximum amount of liquid possible to create a large enough volume for powder incorporation.

In contrast, the DISPERVAC installation, which uses trunk conical-shaped dispersers, allows for a different strategy: taking advantage of the conical bottom to work with the minimum required liquid volume, enabling TiO? to be dispersed more efficiently, achieving better particle size distribution and higher color development.

In a second phase, more liquid is added, followed by the fillers. This two-step sequence, with varying amounts of wetting liquid, optimizes the tinting strength of TiO?.

This sequence can be easily executed using the DISPERVAC control system, allowing for fully programmable stages. By dispersing TiO? first, improved final product quality and reduced TiO? consumption are achieved.


Manufacturing of TiO? slurries and intermediate products

The DISPERVAC system is effective for producing high-quality slurries. The programmable vacuum powder charging system ensures optimal product quality and excellent traceability throughout the manufacturing process.

The continuous slurry manufacturing system can be replaced by a DISPERVAC process using high-capacity dispersing equipment, enabling the production of up to 24 tons of slurry per single formulation. Smaller batches can also be produced with the same guaranteed quality.


Summary of advantages of vacuum pigment charging with the DISPERVAC system:

  • Increases the colour strength of pigments.
  • Allows reduction in the amount of pigment used in manufacturing.
  • Enables complete extraction of manufacturing air before packaging.
  • Reduces manufacturing cycle times.
  • Reduce the amount of defoamer required in the formulation.
  • Permits programmed charging of pigments and dispersants through the control system.
  • Final batches have manufacturing traceability and uniform quality guaranteed by the charging control system.

Conclusion: DISPERVAC, a breakthrough in dispersion and vacuum charging processes

In summary, the DISPERVAC system represents an innovative and efficient solution for the handling and dispersion of powdered raw materials in paint and ink manufacturing. Its vacuum charging technology not only enhances process safety and ergonomics but also optimizes the technical and economic performance of formulations, especially in the handling of critical pigments such as titanium dioxide.

The combination of controlled feeding reduced entrapped air, and the ability to parameterize each operation enables superior final product quality, with greater consistency, lower cost, and improved sustainability. Oliver + Batlle thus reaffirms its commitment to innovation and excellence in industrial processes by delivering solutions that address the current challenges of the sector.


dispervac request information


Innovation and efficiency in pigment incorporation in the chemical sector

SIKA, founded in Switzerland in 1910, is a global leader in specialized chemical products for industries such as construction, automotive, and renewable energy. With operations in over 100 countries, the company stands out for its commitment to innovation, sustainability, and high performance across all its products.

SIKA’s product portfolio includes solutions for concrete additives, waterproofing, adhesives, repair and reinforcement of structures, as well as roofing and facade systems. Their commitment to quality and efficiency has enabled them to maintain a strong presence in the global market.

More information: SIKA

The challenge: Efficient pigment incorporation without compromising quality or efficiency

SIKA needed a solution to incorporate pigments hygienically and efficiently in the production of tinted oil, a key component in several of their products. Proper pigment suspension and dispersion in the oil are essential for ensuring high quality and consistency in the final product.

The specific requirements for the project included:

  • Avoiding dust emission during the operation.
  • Preventing cross-contamination between pigments while working with various shades.
  • Minimizing waste during the pigment incorporation process.
  • Ensuring minimal investment, with a focus on resource optimization.
  • Controlling a finished product viscosity range varying between 100cP and 20,000cP, which adds a challenge to maintaining both quality and flow of the mixture.

The O+B solution: Innovative technology tailored to customer needs

To address this challenge, O+B began with a phase of pilot plant tests to validate the technical feasibility of the proposed solution. These tests were essential for determining the key parameters of the process, focusing on two main aspects:

  • Determining the minimum pneumatic transport speed required to ensure that the pigments were properly transported to the mixer-disperser without losing efficiency.
  • Establishing the maximum speed to avoid the pigments transferring into the liquid, which would cause splashes and possible spillage.

With the results obtained from these tests, O+B proposed an optimized industrial solution that was also economical, involving a vacuum loading and dispersion system to incorporate 8 pigments efficiently and without contamination. This system was implemented in a Dispermix O+B, specifically designed to ensure a hygienic and precise process.

Start-up tests: Performance and efficiency in action

During the start-up phase of the solution, the following data was verified:

  • 300 kg of gray pigment incorporated in 20 minutes, meeting the system’s expected capacity.
  • Only 100 g of solid pigment passed through the filter, representing an 0.03% loss, an exceptionally low figure that highlights the efficiency and precision of the system.

    These tests confirmed that the system was highly efficient, maintaining the quality standards required by SIKA.

Results achieved: Performance, hygiene, and efficiency

The system implemented by O+B has allowed SIKA to achieve efficient pigment incorporation without contamination, resulting in a cleaner production process with minimal waste. The outcomes are as follows:

  • Reliability in the process, with controlled pigment incorporation.
  • Resource optimization, significantly reducing waste in the process.
  • Compliance with SIKA’s stringent quality standards, ensuring a homogeneous and consistent product.
  • Constant and safe performance, with a fully automated system that provides greater process control.
  • High operational efficiency, improving productivity and reducing downtime.

The technology implemented not only guarantees constant and secure performance but also optimizes the efficiency of every phase of the production process, from initial loading to final dispersion.

This project demonstrates how O+B can deliver innovative and tailored solutions that enhance quality, efficiency, and sustainability in industrial processes. The implementation of this technology has strengthened SIKA’s commitment to excellence, ensuring the highest quality in the production of tinted oils and other products.


accessories for the automation

A high-precision project in the heart of the cosmetics industry

COBELSA Cosméticos S.A., located in Alcalá de Henares (Spain), is part of the L’ORÉAL Group and specializes in the production of nail polish for international brands such as Maybelline and Color Riche. All production is destined for markets in Europe, Brazil, and the United States.

As part of its continuous improvement strategy, COBELSA turned to Oliver + Batlle to develop a new manufacturing unit for bentone gel, a key ingredient in nail polish formulas, acting as a rheological agent that ensures the suspension and stability of pigments and resins.

The challenge: safety, precision and automation in a confined ATEX zone

The project came with several critical technical challenges:

  • Extremely limited installation space
  • Location in a classified ATEX II GD zone, due to the presence of solvent vapors and bentonite dust
  • Vacuum powder feeding of explosive bentonite into a flammable medium (butyl acetate + nitrocellulose)
  • Manufacturing process requiring a permanently inert atmosphere (O? < 6%) to prevent premature drying
  • A fully automated and traceable control system

O+B was tasked with delivering a compact, safe and high-performance solution tailored to these conditions.

O+B’s solution: compact engineering in a skid-mounted system

O+B’s technical team designed a complete and autonomous skid, optimized for integration into the ATEX environment and adapted to the space constraints of the plant, consisting of:

Working platform

1. POLIMIX DPS-1200-OR Disperser

  • ATEX Zone 0 certified (internal)
  • Weighing system via load cells
  • Half-coil cooling jacket, product temperature probe and minimum level sensor
  • CIP cleaning system with automatic motorized lance
  • Liquid input via multi-way feed collector

2. Bentonite powder hopper

  • Stainless steel AISI 304, capacity 150 L
  • Vacuum suction lance for 25 kg bags
  • Vacuum monitoring via manovacuum gauge
  • Percussion hammer for complete discharge

3. Vacuum powder feeding system

  • Flameproof filter above the disperser
  • Flame arrestor + modulated vacuum valve
  • Side channel vacuum blower
  • Acid dispersion input by vacuum

4. ATEX safety & inert gas control

  • Grounding verification system for all components


  • Nitrogen inerting system (N2)

  • Oxygen monitoring sensors in both disperser and powder hopper

5. Fully automated control system

  • ATEX-rated HMI touchscreen in classified area
  • SCADA system in a safe zone with integrated recipe manager


Results: enhanced quality and safe, controlled production

The solution developed by O+B enabled COBELSA to:

  •  Comply with the most demanding ATEX safety standards
  •  Eliminate manual handling of explosive powders
  •  Maintain a stable inert atmosphere (O? < 6%) during the process
  •  Achieve higher gel quality compared to previous systems
  •  Fully automate and digitize the gel manufacturing process

This project demonstrates how modular engineering and technical expertise allow O+B to overcome complex challenges in sensitive environments. With this solution, O+B strengthens its position as a trusted technology partner in the cosmetic industry, where process control, product consistency, and safety are non-negotiable.


accessories for the automation

A new O+B Success story for Nippon Paint

A global client with a long-term vision

Founded in 1881, Nippon Paint is one of the world’s leading companies in the manufacturing of paints and coatings. With over 140 years of history, the Japanese company operates in more than 30 countries, offering innovative solutions for sectors as diverse as decorative, industrial, automotive, and marine paints.

In China, Nippon Paint has built a robust industrial ecosystem with plants specializing in the production of water-based decorative paint. These facilities are designed to meet the demands of a dynamic and highly competitive market, where production efficiency, automation, and environmental respect are key factors.

More information: nipponpaint-holdings.com/en/


The challenge: 30 tons of decorative paint per hour

The project’s objective was clear and ambitious: to design and install an automated line capable of manufacturing and packaging 30,000 kg of white decorative paint (water-based) per hour, with maximum reliability and precision. This was the third consecutive project that O+B carried out for Nippon Paint in China, following two similar installations in Xianning (Hubei) and Zhengzhou (Henan). This continuity reflects the client’s confidence in our ability to deliver high-performance turnkey industrial solutions


O+B’s technical solution: Comprehensive process automation

The project was developed based on a modular, highly automated solution that encompasses everything from raw material handling to final product packagingEach stage of the process was designed to maximize performance and ensure complete traceability

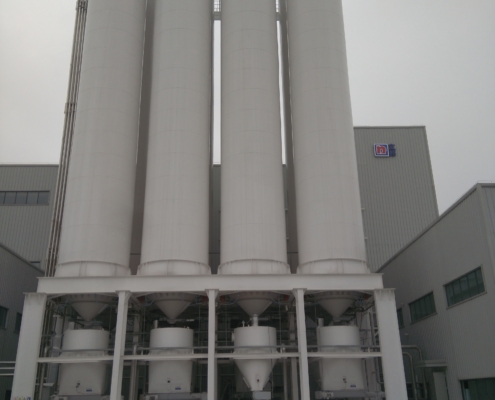
1. Raw material storage eight 300 m³ silos were installed to store powdered raw materials such as calcium carbonate, kaolin, talc, and titanium dioxide

2. Automatic transport and dosing of solids

A pneumatic transport system with a capacity of between 15 and 30 tons per hour feeds two waiting hoppers. Each hopper is dedicated to a group of raw materials: one for carbonate, kaolin, and talc, and another exclusively for TiO?, allowing for separate and precise management.

3. Automatic liquid dosing

The automated system manages the dosing of 18 emulsions and 40 liquid additives, ensuring precision, repeatability, and reduction of human errors.

4. Solid dispersion and mill base manufacturing

The critical mixing stage is carried out with a POLIMIX DPS-15000-OR coaxial disperser, capable of simultaneously incorporating solids from both hoppers. Its dispersion capacity of up to 50 tons per hour ensures very short cycle times and perfect product homogeneity.


5. Discharge and final homogenization

The mill base is discharged by gravity into two TA-22000 finishing tanks, designed to receive large volumes with continuous agitation, ensuring uniform mixing before packaging.


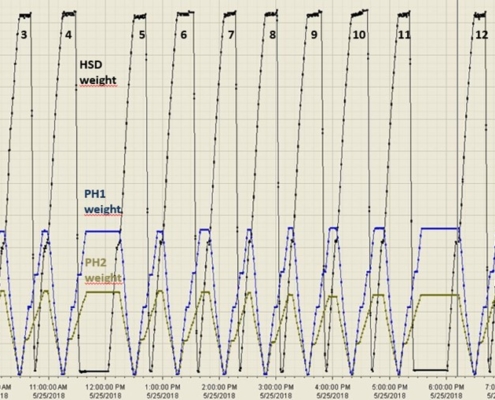
6. Performance validation

The analysis of the actual weight in the DPS-15000-OR and the two solid hoppers throughout a workday demonstrates that the system is capable of producing 30,000 kg of paint in less than 60 minutes, thus meeting the set objective.


7. High-speed automatic packaging

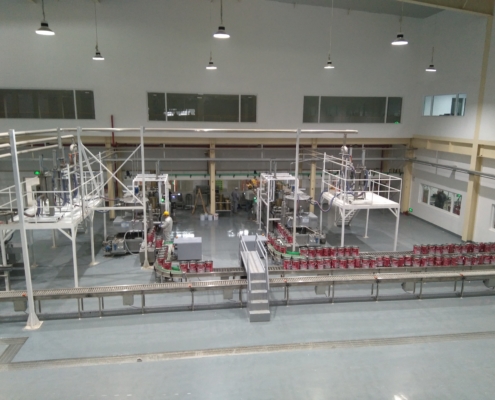
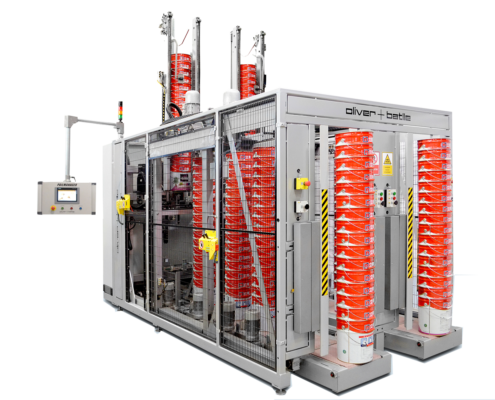
The finished paint is packaged using two automatic FLASH-25-TX lines, each equipped with PAILMANAGER-VX systems for feeding and handling 18-liter containers. This system allows a packaging rate of 14 containers per minute per line, with quick format change and minimal manual intervention.


INTRODUCTION

At Oliver + Batlle, we offer a wide  range of specialized machinery for the production of water-based phytosanitary products, a format that is increasingly in demand in the industry due to its advantages in handling, safety, and efficacy.

Among the pesticide products processed under this system, we find:

  • Herbicides and algaecides: for weed control.
  • Insecticides and acaricides: for combating insect pests.
  • Nematicides: aimed at eliminating soil-borne diseases in crops.
  • Fungicides: such as the common copper oxychloride, for controlling fungi.
  • Fertilizers and growth products: to promote crop development.

In the past, these products were supplied in powder form, which posed significant risks of contamination, dirt in handling areas, and inhalation toxicity. The evolution towards liquid formulations has eliminated these drawbacks, enabling the production of concentrated suspensions or flows, which are much safer and more efficient.

Advantages of liquid pesticide products:

  • Cleaner and easier handling compared to powder products.
  • Easier and more accurate application dosing.
  • More efficient storage in drums.
  • Greater biological activity compared to powders.
  • Better distribution of active particles in the liquid medium.
  • More uniform particle size.
  • Allows for simpler and more efficient cleaning of application equipment.

Liquid bases used in formulations:

  • Water
    • Solvents (currently being phased out for environmental and safety reasons)
    • Water and solvent mixtures: where each phase is prepared individually before mixing.
  • Oil

To carry out the production of these products, Oliver + Batlle offers equipment for all stages of the process:

  • Dispersion
  • Grinding
  • Finishing
  • Filtration
  • Filling

Below, we detail each of these stages and the machinery available in our program to ensure maximum efficiency and quality in the production of water-based phytosanitary products.


DISPERSION

The dispersion phase is essential in the production of water-based phytosanitary products as it ensures the homogeneous incorporation of the active ingredient along with the additives and liquid components of the formula.

Common components in dispersion:

  • Active ingredient (or technical grade), generally in powder form.
  • Liquid medium: water, solvent, oil, or combinations of these.
  • Glycol or paraffin oil: between 2% and 8%.
  • Dispersant: in proportions of 2% to 10%.
  • Wetting agent: between 0.5% and 3%.
  • Antifoam agent: around 0.1% to 0.5%.
  • Thickener: added between 0.2% and 0.4%, previously prepared in a 2% aqueous solution to ensure proper dilution and avoid the formation of lumps or gels.

In some formulations, high-purity silica may be added as a rheological modifier.

The active ingredient must be incorporated into the liquid medium using a mixer-disperser, which ensures its proper dispersion and prevents the formation of clumps.

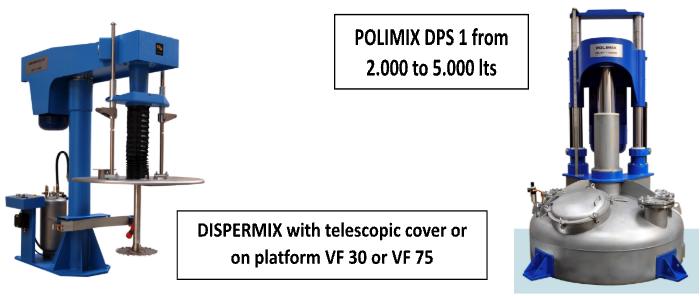
Recommended equipment: To perform dispersion, equipment from the DISPERMIX range is primarily used,  sized with the required power according to the batch volume:

  • From portable models to platform versions for higher-capacity productions.

Over time, due to the need to improve working conditions, avoid operator exposure to harmful dust, and protect the environment, the use of closed systems such as POLIMIX has been incorporated. These systems, with specific installations for raw material feeding, guarantee a safer and cleaner working environment.

POLIMIX can be:

  • Single-shaft dispersers.
  • Coaxial models equipped with wall scrapers, ideal for high-viscosity products and complex formulations.

Recommended turbines and working conditions:

  • Sawtooth turbines or HDM (High Dispersion Mixing) type.
  • Optimal peripheral speeds: between 24 and 28 m/s.
  • The diameter of the tank should be 2 to 3 times the diameter of the turbine to ensure proper fluid dynamics.

Formulation parameters:

  • Powder solids concentration: Generally between 30% and 70% by weight.
  • Common viscosity of the mixture: Usaully between 800 and 1,200 cPs. With these characteristics, the standard power of each machine model assigned according to batch size is sufficient without the need for over-sizing or using higher-power equipment.

Design and materials of equipment: Dispersion tanks should be made of AISI 316 L stainless steel and feature cooling jackets.

Temperature recommendations:

  • Temperature of the coolant: below 4 ºC.
  • Maximum process temperature: should not exceed 30 ºC to protect heat-sensitive active ingredients.

Foam control: In this type of formulation, foam formation during dispersion is common. If this issue is detected and working with a POLIMIX system, it is recommended to use the vacuum loading system, which minimizes foam generation and improves process efficiency. This aspect should be adjusted according to each product and validated during initial testing.


GRINDING

In the grinding phase, the separation of active ingredient particles that were not fully disaggregated during dispersion takes place. Additionally, some active ingredients may undergo a particle fracture process, resulting in smaller particle sizes. This stage is crucial to ensure that phytosanitary  products meet regulatory standards and technical specifications, such as CIPAC regulations for pesticide products.

One of the key objectives in this process is to ensure that 50% of the particles are smaller than 5 microns, and 90% are smaller than 10 microns, guaranteeing the quality and effectiveness of the products.

Available types of mills:

  • Continuous mills:  SUPERMILL.
  • Batch mills: MILL-ENNIUM.

Both types of mills are effective for particle disaggregation. While the Supermill generates shear forces within its milling chamber, the Mill-enium combines shear forces and impact, providing better energy transmission and a significant advantage in terms of production capacity.

Comparison of results in tests: In tests carried out with copper oxychloride, both machines showed comparable quality results, but with differences in energy consumption and manufacturing time. The data was as follows:

  • Mill-enium RS-20 (copper oxychloride): 0,06 kW/lt.
  • Supermill EHP-50 (two passes of copper oxychloride): 0,259 kW/lt.

This implies an energy savings of 77% when using the Mill-enium compared to the Supermill. Additionally, in terms of manufacturing time, the Mill-enium RS-20 would process 1,100 liters in 67 minutes, while the Supermill EHP-50 would need 330 minutes, resulting in an 80% time saving.

Granulometry characteristics of products:

  • For initial particle sizes between 150 and 200 microns, two passes are required to achieve sizes smaller than 5 microns.
  • For initial particle sizes between 40 and 50 microns, one pass is sufficient to reach sizes smaller than 5 microns.


Summary of operating parameters for both machines:

Supermill EHP:

  • Materials in contact with the product: Duplex stainless steel.
  • Feeding pump: Gear or helical stainless steel AISI 316L, with adjustable speed.
  • Grinding shaft: Belt transmission, electric motor with adjustable speed.
  • Grinding balls: Zirconium 1.8-2.0 mm in the first pass, and 1.2-1.4 mm in the second.
  • Grinding chamber: Provided with cooling jacket,  with water supply at 4°C.

Mill-enium RS:

  • Materials in contact with the product: Stainless steel AISI 316L or Duplex.
  • Grinding shaft: Tungsten carbide peg and counterpeg system, turbo-type turbine.
  • Grinding elements: Yttrium (0.7-0.9).
  • Grinding basket: Cooling recirculation system, process vessels with cooling jacket, water at 4°C.

Pumping and filtration: Between milling and finishing, product pumping through a pumping and filtration group is required. This process should be done with a pneumatic pump and a bag filter. The objective is to remove coarse raw material particles and milling balls, so it is recommended to use a monofilament nylon bag with 50-micron filtration.


FINISHING OR STORAGE OF PRODUCT

Once the product has passed through the milling phase, it will be stored in a tank, with the tank capacity determined by the plant’s production volume. It is essential that this tank is equipped with an efficient agitation system to ensure the homogenization of multiple production batches and, if necessary, the addition of additives such as thickeners to adjust the formula.

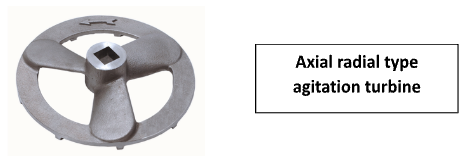
The most suitable type of agitation for this process is a mixer equipped with radial axial turbines, with an off-center shaft in the tank. For tanks with capacities exceeding 5,000 liters, it is recommended to install a second radial axial pumping turbine without dispersion hammers, which facilitates the incorporation of prefabricated thickeners.

Additionally, these tanks should be designed with variable speed, allowing the adjustment of the agitation speed according to the rheological characteristics of the product, ensuring its homogeneity. As in other stages of the process, the parts in contact with the product should be made from AISI 316L stainless steel to avoid contamination.


PUMPING AND FILTRATION

Before proceeding to filling, the product must be pumped using an appropriate pumping system that includes a filter to ensure that the final product delivered to the customer is free of impurities from the manufacturing process.

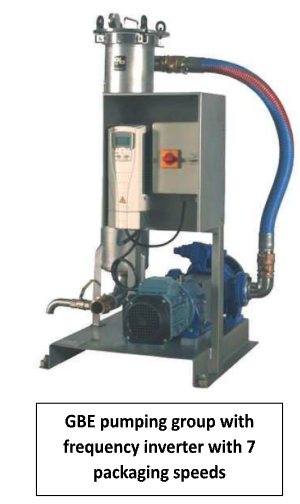
A recommended universal base equipment is the GBE Electric Pumping Group, which includes a pump made of AISI 316 stainless steel and an AGF 51 or AGF 53 bag filter with 5-micron filtration. Since many phytosanitary  products tend to generate foam during the filling process, the pumping system must include a speed selector. This way, a slow filling  speed can be set at the beginning of the process, and once the filling nozzle is submerged, the filling speed can be increased.


FILLING SYSTEMS

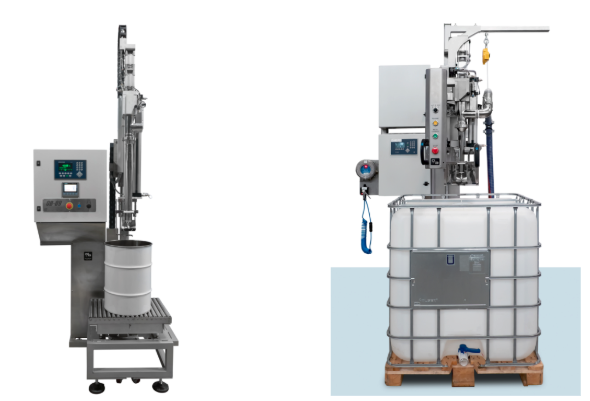
The most common containers in the agrochemical industry are 5 and 10-liter polyethylene drums. To fill these containers, a gravimetric filling system with a submersible  headstock, such as the OB-DRUM model, can be used . It features a scale up to 25 kg, and a filling nozzle of the appropriate diameter for the type of drum to be filled.

If production increases and the number of containers to be filled is considerable, the PALET-1500 model, fitted with a rotary headstock can be used. This system allows packaging groups of drums placed on pallets, optimizing production capacity and workflow.


Tests Performed in O+B Laboratory with Phytosanitary  Products:

  • Active Ingredient: Copper Oxychloride
  • Pyrimethanil
  • 80% Sulfur
  • 93% Sorbitol
  • 24% Oxifluorfen


CONCLUSION

In summary, the production of phytosanitary  products in aqueous suspension offers numerous benefits over powder formats, especially in terms of safety, efficacy, and ease of handling. Oliver + Batlle offers an integrated solution throughout the entire production process, from the dispersion of active ingredients to the final product packaging. Thanks to its range of specialized machinery, manufacturers can ensure more efficient production with optimal quality control in a safe environment for both operators and the environment.

Oliver + Batlle’s commitment to innovation and advanced technology ensures that production plants can maximize their capacity, reduce energy consumption, and improve the quality of the final product. Additionally, laboratory tests support the effectiveness of their solutions for processing complex active ingredients, such as copper oxychloride, pyrimethanil, and other common compounds in the phytosanitary  industry.

In an increasingly competitive and demanding sector, choosing the right machinery is essential to optimize resources and comply with regulations. Oliver + Batlle positions itself as a key ally in the manufacturing of phytosanitary  products in aqueous suspension, offering solutions that meet the highest standards of quality, safety, and sustainability.