EUROTEX: Manufacturing and marketing of industrial and decorative paints, and waterproofing products

EUROTEX began its business activity in the early 1980s as a specialized paint store in Mairena del Alcor, Seville. In 1987, aimed at gaining greater control over its production processes, the company started manufacturing the products it sold and established its factory and headquarters in El Viso del Alcor.

Currently, EUROTEX manufactures and markets a wide range of products, including industrial and decorative paints, primers, sealers, and waterproofing materials.

What product does the plant manufacture?

The project was focused on the manufacture of water-based paints and other water-based products.

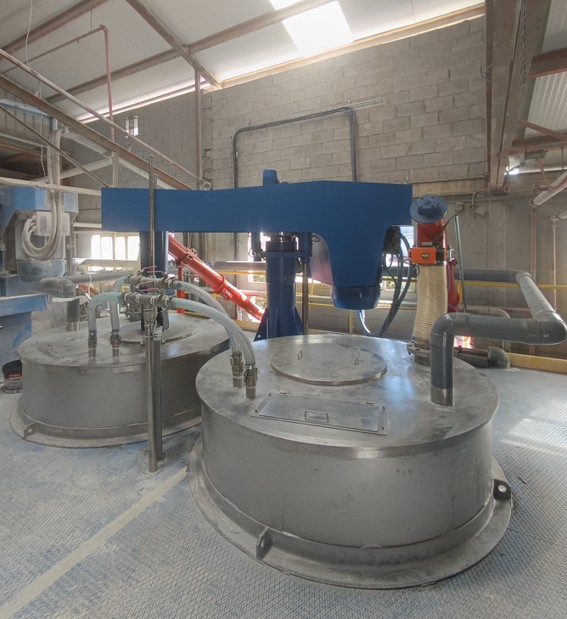
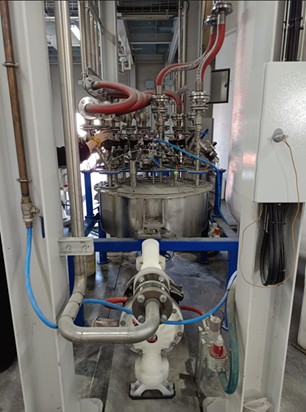
The process is carried out in two tanks, where the dispersion and finishing stages of the formulation take place. The product then passes through a pumping and filtration system before filling.

The Challenge: Design and integrate a new water-based coating production unit

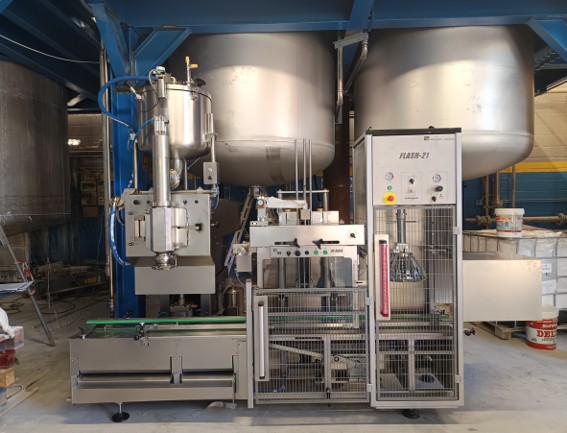
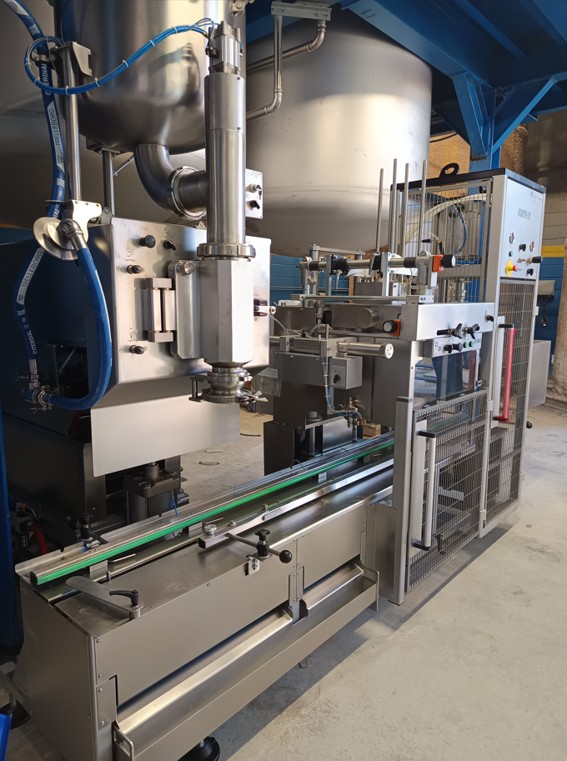
EUROTEX needed to install a new production unit for water-based products, consisting of a Dispermix VF-132-E high-speed disperser, two DE-7200 tanks, an MF-16 pumping and filtration unit, and a FLASH-21 volumetric filling machine.

The project presented three main constraints:

  • Tight Delivery Schedule: The installation had to be operational prior to the start of the production campaign, requiring a particularly demanding delivery schedule.
  • Limited Available Space: The new unit had to be integrated into an area with space and height restrictions. O+B designed a dedicated platform to accommodate the manufacturing equipment, taking into account the existing access points, its connection to an existing platform, and pallet access through safety gates.
  • Integration with third-party systems: The dispersion equipment had to be integrated with the solid and liquid feeding systems supplied by another vendor, requiring coordination among the different parties involved.

Oliver+Batlle’s Solution: A coating manufacturing unit tailored to space and process needs

Industrial machinery supplied for the production process

To meet the project requirements, O+B supplied the following equipment:

  • Industrial disperser: One Dispermix VF-132-E, equipped with a motorized crown for automatic head rotation, a telescopic cover with blade access port, an HDM Ø675 mm dispersion blade, and a bag support tray.
  • Process tanks: Two DE-7200 tanks to be installed on the platform, configured with a loading manhole and the necessary connections for powder and liquid addition, as well as dust extraction.
  • Pumping and filtration system: One MF-16 pneumatic pumping and filtering unit, designed for pumping and filtering the product manufactured in the DE-7200 tanks prior to filling.
  • Automatic filling line: One FLASH-21 volumetric filling machine, featuring a TA-100-HD hygienic hopper, NE-20 electronic level sensor, AV-20 valve with actuator, SLT-20 cleaning system, and DT-350 lid dispenser.
Plant layout engineering, assembly, and commissioning

In addition to supplying the equipment, O+B developed the plant layout engineering for the various elements located both above and below the platform: disperser, DE-7200 tanks, pumping unit, and automatic volumetric filling machine.

To accurately define the equipment layout, site measurements were taken beforehand, and construction drawings for the manufacturing platform were prepared and agreed upon with the client.

The platform was designed and engineered by O+B and manufactured and installed by a third party.

Mechanical assembly of the equipment was carried out by an O+B technician. Moving the disperser and tanks into position posed an additional challenge due to the limited space and height available, requiring close coordination with the crane contractor appointed by EUROTEX.

Electrical and pneumatic installation works were carried out by the client and subsequently supervised by an O+B technician.

Finally, O+B carried out the plant commissioning, starting up and adjusting the machines for normal operation.
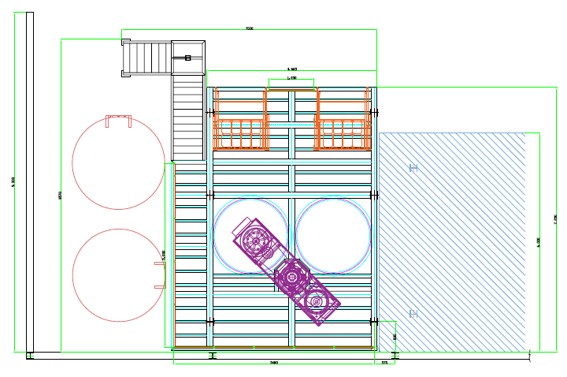
Platform layout drawing designed and calculated by Oliver + Batlle
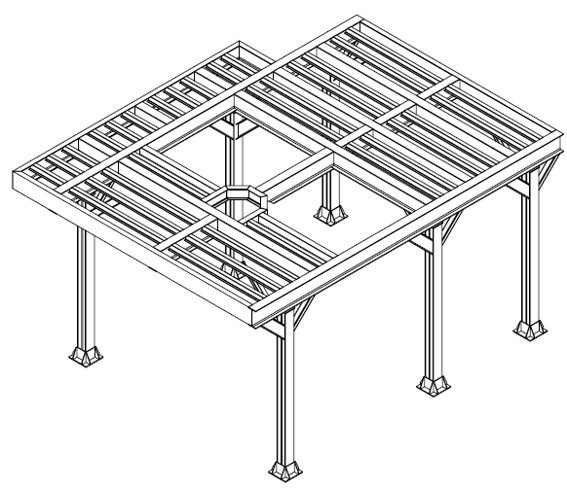
3D structural drawing of the platform
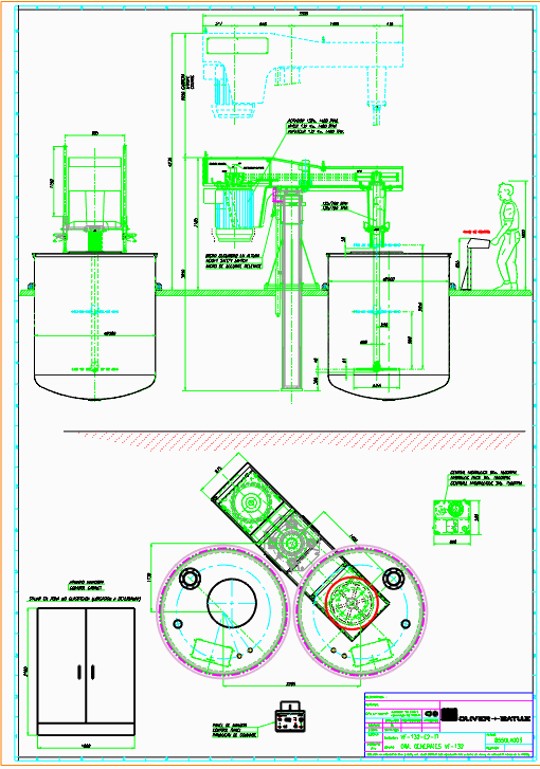
Plant layout drawing of the Dispermix VF-132-E and two DE-7200 tanks

Project Results

The new manufacturing unit enables EUROTEX to produce water-based coatings and meet customer demands in terms of both quality and turnaround times.

One of the main operational advantages of this configuration is the ability to stagger production and filling between the two tanks: while a batch is being filled from one tank, production of another batch can begin in the second tank.

This increased operational flexibility substantially enhances the plant’s overall production capacity.

Are you planning to expand your plant or add a new water-based paint manufacturing line?

At Oliver + Batlle, we specialize in the design and execution of custom process engineering projects for the paint and coatings industry. We develop turnkey solutions for the manufacture of water-based paints, varnishes, adhesives and inks, integrating dispersion equipment, filtration systems, filling lines and working platforms to maximize the efficiency, safety and productivity of your facilities.

Get in touch with our engineering team today to find out how we can help you expand your production capacity and integrate new equipment into your plant without disrupting your operations.
Space and headroom constraints are among the biggest challenges paint manufacturers face when trying to scale up production. When conventional silos or hoppers simply won’t fit, manufacturers need highly customized engineering solutions that can boost output without touching the building structure. In this success story, we explore how Oliver + Batlle optimized solids feeding and pneumatic conveying for manufacturer Alliance Maestria, eliminating production bottlenecks and quadrupling capacity within a severely restricted vertical space.

Alliance Maestria: Innovation in Decorative Paint Manufacturing

Alliance Maestria is an independent paint manufacturer headquartered in France, specializing in the development and production of coatings for a wide range of industrial applications. Their portfolio spans decorative solutions, flooring systems, anti-corrosion coatings, and road marking products, all formulated to meet varying regulatory and performance requirements.

For this particular project, the scope centered on optimizing the manufacturing processes for water-based decorative paints.

The product being manufactured is water-based decorative paint,a product where precise control over process conditions is critical to ensuring stability, consistency, and final quality.

The Challenge: Maximizing Solids Discharge in a Constrained Vertical Space

The primary technical constraint was the limited headroom in the dispersion area, which ruled out the use of conventional large-volume solids discharge hoppers.

This meant rethinking the entire raw material feeding system from scratch, finding a compact vertical solution that wouldn’t compromise process performance.

Alongside this, production requirements demanded high discharge flow rates in line with contractually agreed targets:

  • Carbonates: 15–18 t/h 
  • Titanium dioxide (TiO2): 10–12 t/h 

The technical challenge was therefore to engineer a dosing system that could perform within highly restricted spatial conditions, matching or exceeding the feed rates of conventional hoppers while delivering continuous, stable, and controlled solids discharge.

The Oliver + Batlle Solution: Integrated Automation and Pneumatic Conveying

Oliver + Batlle designed and implemented a comprehensive engineering solution aimed at making the most of the available space while fully meeting production requirements. The solution brings together solids handling, liquid dosing, dispersion, and packaging systems — all integrated under a single framework of advanced automation.

High-Efficiency Cyclonic Hopper System

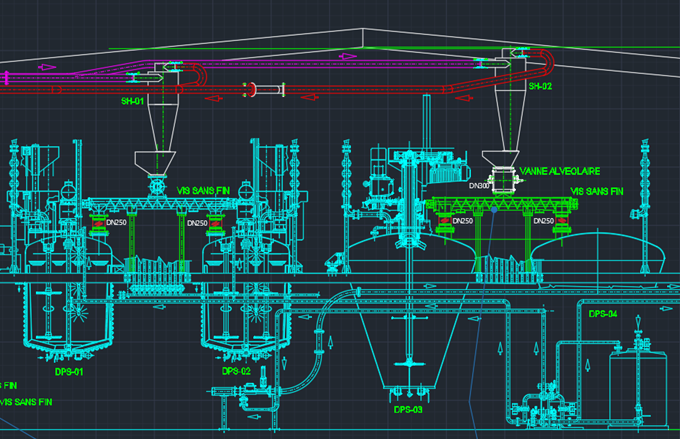
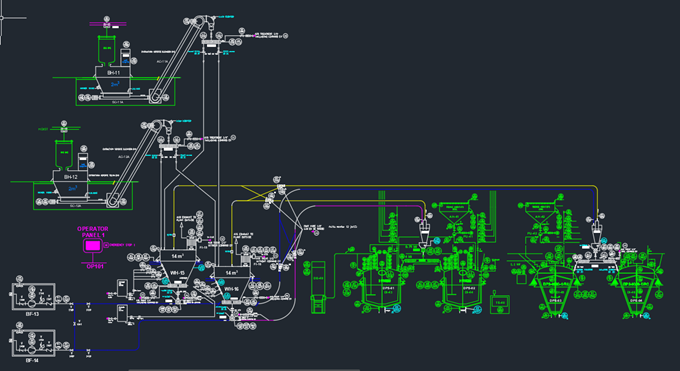
Two cyclonic hoppers (SH-01 and SH-02) were installed at the highest available elevation, making full use of the vertical space. These hoppers deliver continuous, controlled solids discharge directly onto the dispersers:

The cyclonic geometry promotes the flow of cohesive materials, minimizing bridging and caking risks while sustaining continuous, high-rate discharge in space-constrained conditions.

Closed-Loop Pneumatic Conveying (Loop System

Solids transfer relies on dilute-phase pneumatic conveying in a closed-loop configuration, moving material from 14 m³ floor-level storage hoppers (WH-01 and WH-02) up to the cyclonic hoppers.

This design delivers:

  • Zero dust emissions: the system is fully enclosed 
  • Improved safety and housekeeping conditions 
  • Continuous, stable feed to the dispersers

Precise Liquid Additive and Emulsion Dosing

A dedicated system was put in place to handle liquid additives and emulsions, built around 250 L weighing hoppers and automatic distribution manifolds.

This system enables:

  • Precise, repeatable dosing of critical components 
  • Flexible feeding to both dispersers and finishing tanks 
  • Full integration into the process control logic

100% Automated Finishing and Packaging Lines

The installation is rounded out by a system for fully automated product finishing and conditioning:

Finishing tanks:

  • 4 units of 16,000 L 
  • 2 units of 11,000 L 

Fitted with high-precision Mettler Toledo weighing systems and CIP cleaning via rotary spray heads.

Packaging lines:
Two automatic volumetric filling lines, Flash 21, designed for precision, repeatability, and high production throughput.

Operational and Safety Improvements

In a subsequent project phase, further upgrades were introduced to boost system reliability and working conditions:

  • Replacement of vibration-based systems with Airsweep technology to improve solids discharge in large-volume hoppers 
  • Automation of packaging line cleaning cycles using dedicated Siemens S7-1200 PLCs 
  • Installation of a Big-Bag handling system with a 2,000 kg hoist, improving ergonomics and reducing operational hazards

Together, these improvements eliminated the constraints of the previous system and established a robust operational foundation capable of meeting , and exceeding, the flow rate and productivity targets defined in the project.

Arc-En-Ciel Project Results: Greater Profitability and a Cleaner Plant

The implementation of the Arc-En-Ciel project has delivered a significant step forward in operational performance, particularly in terms of conveying capacity, cycle time reduction, and overall process efficiency.

Significant Increase in Conveying Flow Rates

The closed-loop pneumatic conveying system, combined with the cyclonic hoppers, has not only met but surpassed the contractual targets:

  • Calcium carbonate (CaCO3): hasta 20 t/h (objetivo: 18 t/h) 
  • Titanium dioxide (TiO2): hasta 17 t/h (objetivo: 12 t/h) 
  • Talc: up to 11 t/h 

These figures represent a substantial improvement over the previous system, eliminating the bottlenecks caused by poor solid-air separation that had been restricting flow rates and causing material losses.

Reduced Cycle Times and Higher Productivity

The higher feed rates have made it possible to quadruple solids feeding capacity to the dispersion stage, significantly cutting batch loading times and, by extension, total process time.

The knock-on effects are tangible:

  • Higher plant throughput 
  • Less idle time in the dispersion stage 
  • Improved overall equipment effectiveness (OEE)

Better Product Containment and Working Conditions

The switch to a closed-loop conveying system has eliminated dust emissions and the material losses associated with traditional filtration-based systems.

On top of this, integrating pigging (pipe cleaning) transfer systems on the mill-base lines has made it possible to:

  • Maximize product recovery 
  • Reduce waste 
  • Improve cleaning efficiency and process traceability

Expanded Parallel Operating Capacity

The system architecture — with independent conveying lines including duplicated storage hoppers, blowers, and cyclonic hoppers — enables simultaneous feeding of two dispersers, effectively doubling the plant’s operational capacity at the solids loading stage.

Technical Assessment: Eliminating Manufacturing Bottlenecks

  • Elimination of the main process bottleneck (solids feeding) 
  • Simultaneous improvement across capacity, operational efficiency, and cleanliness
  • A step change from a design-limited system to a robust, scalable solution fit for demanding production environments

Is your production plant facing space or capacity challenges?

At Oliver + Batlle, we specialize in designing bespoke process engineering projects for the paint and coatings industry. We optimize your facilities to achieve maximum efficiency and profitability. 

Get in touch with our engineering team today and find out how we can help you overcome your production bottlenecks.

Puma Group and its coatings division

Grupo Puma  is a leading business group in the construction materials sector and the largest manufacturer of mortars in Spain. With over 40 years of experience, it develops a wide range of solutions for construction, including adhesives, insulation systems, flooring, asphalt products and renovation solutions.

The group also has a division specialising in coatings, both water-based and solvent-based, for the manufacture of waterproofing and decorative paints for façades and fillers that can be applied to different surfaces. It currently has 37 production centres and a distribution network spanning four continents.

Product to be processed and project objective

The client manufactures coatings and coverings mainly for the construction sector. Within the framework of this project, the installation of additives is intended for the production of water-based coatings.

The incorporation of additives during the manufacture of paints and coatings is common practice in the industry, as they allow various properties of the final product to be adjusted and improved. Their functions include improving the dispersion of pigments and fillers (dispersants), controlling foam generated during the process (defoamers), stabilising the system by adjusting the pH, and providing specific properties such as biological resistance, gloss control, or modification of drying times.

These additives are normally used in small quantities and are incorporated at different stages of the manufacturing process, which requires precise and repeatable dosing to ensure the quality and homogeneity of the final product. They are usually supplied in industrial containers such as IBCs or 200-litre drums, so in many plants weighing and addition are done manually.

In this context, the aim of the project was to design and implement an automated system capable of managing the weighing and precise dosing of different additives into eight independent dispersion tanks. The installation had to guarantee speed, accuracy and repeatability in the additions, integrating into the existing production process and allowing the direct use of IBCs as storage tanks for the additives. The aim was to avoid frequent transfer or replacement of containers, optimise internal raw material logistics and improve the overall efficiency of the manufacturing process.

Oliver + Batlle solution

To solve the challenge, Oliver + Batlle designed an automated additive dosing system comprising the following main elements:

  • A 300-litre additive weighing hopper, made of stainless steel and equipped with load cells. It incorporates automatic valves for dosing 11 different additives: 9 of them dosed by gravity and 2 by pumping, due to their higher viscosity. The system also has manual valves with micro-switches for loading the stock IBCs of each additive.
  • Two pneumatic pumping units, designed for dosing higher viscosity additives.
  • A pneumatic transfer pump, responsible for transferring the product from the weighing hopper to any of the eight possible destinations.
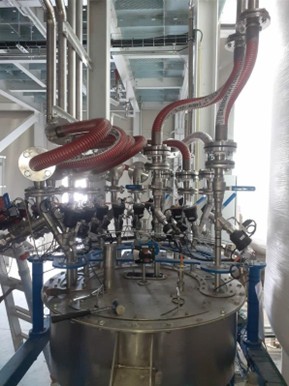
  • A stainless steel distribution manifold equipped with seven automatic three-way valves, allowing the destination of the additive to be selected.
  • Eight automatic line shut-off valves, installed at the inlet of each of the dispersion tanks.
  • An electrical control and manoeuvring cabinet, equipped with a PLC and HMI touch screen, from which the operator can select the additive to be dosed, define the weight set point, manage stock loading and monitor the operation of the installation.
  • Two portable pump units on trolleys, designed for loading IBCs of additive stock.

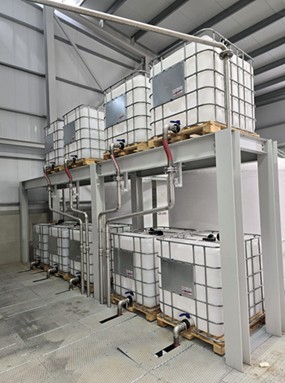
Oliver + Batlle carried out all the engineering work for implementation at the plant, including the distribution of the additive IBCs, the weighing hopper, the pumping equipment and the layout of the pipes from the hopper to the collector and from there to the dispersion tanks.

The mechanical, electrical and pneumatic assembly was carried out by the customer themselves, under the supervision of an O+B technician.

Subsequently, the installation was commissioned with the participation of a mechanical technician and an Oliver + Batlle programmer.

During operation, additives compatible with each other are dosed and weighed in the hopper, from where they are automatically transferred to the selected dispersion tank. The system also incorporates a water cleaning cycle for the hopper and  flushing of the pipeline, ensuring that all the additives reach its destination.

The additive dosing control system was integrated into the factory’s automated system for executing complete recipes using the customer’s SCADA, establishing communication between the PLC of the system supplied by Oliver + Batlle and the plant’s main PLC.

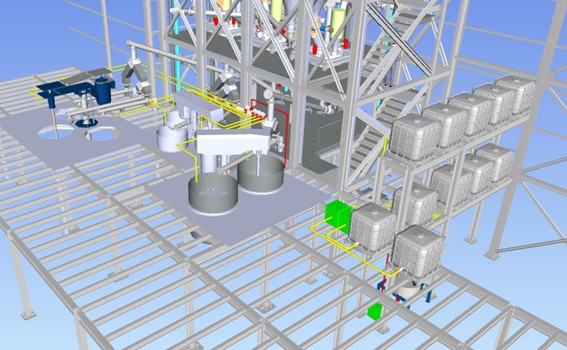
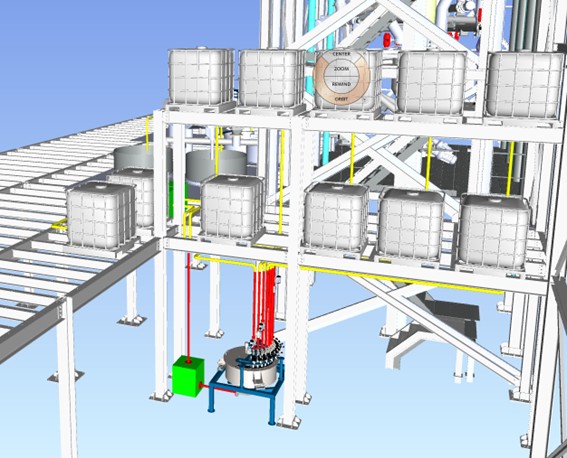
3D views of the additive storage and distribution system: stock IBCs, 3-way valve manifold and piping to dispersion tanks

Results and advantages of the implemented solution

Thanks to the implementation of this automated additive dosing system, the customer has significantly optimised manufacturing times.

The process has gained in precision, cleanliness and repeatability, eliminating the variability associated with manual dosing.

In addition, the system provides complete traceability of the process, recording the dosages carried out for each batch, including the additive code, target value, actual dosage value, destination, date and time of the operation.

Automation has also reduced the operational workload, minimising manual interventions and facilitating the work of the plant operator.


The main advantages of the implemented solution are:

  • Automation of the additive dosing process.
  • Greater precision and repeatability in each manufacturing batch.
  • Optimisation of process times.
  • Improved cleanliness and order in the plant.
  • Complete traceability of dosages performed.
  • Reduction in operator workload.
  • Integration with the existing control system through communication between PLCs.
  • Direct use of IBCs as additive stock tanks, optimising internal logistics.

Do you need to automate dosing in your production plant?

At Oliver + Batlle, we specialise in process engineering design and customised automation for the chemical and coatings industry. From upgrading existing lines to designing turnkey production plants.

Contact our technical team today  and find out how we can help you optimise your cycle times, improve traceability and make your manufacturing process more profitable.

Oliver + Batlle presents the new frontier in paint dispensing and packaging: the Additive Manufacturing 3D Nozzles service, custom-designed for each customer and need.

This approach transforms the concept of a simple product into a completely personalised service optimised for your production line.

Key advantages of the service

Our service transforms the concept of a simple component into a comprehensive customised solution, designed to maximise the performance of your production line based on the following pillars:

  1. Manufacturing efficiency and profitability
  • Increased speed: Achieve up to a 20% increase in manufacturing speed compared to conventional metal dispensers.
  • Time optimisation: Reducing the dispensing cycle is the key factor in increasing your total production capacity.
  • Cost reduction: Operational efficiency and the possibility of accessing annual supply contracts allow for a significant reduction in maintenance and replacement costs.
  1. Dosing quality and filling accuracy
  • No more drips and foam: The customised design ensures perfect flow even with difficult-to-fill products, eliminating common problems with standard nozzles.
  • A nozzle for every container: We implement the concept of an optimal diameter for each type of container, ensuring a millimetre-perfect fit that dramatically improves packaging quality.
  1. Customisation and material superiority

Thanks to additive manufacturing (3D printing), we design nozzles layer by layer with benefits that are impossible to achieve through traditional machining:

  • Minimum weight: Geometric optimisation allows for much lighter parts, facilitating handling and reducing mechanical stress on equipment.
  • Maximum impact resistance: We use advanced technical polymers that offer superior durability against shocks and intensive use in the plant.
  • Ad-hoc flexibility: We adapt each design to the exact specifications of your product and container after a preliminary study of your lines.

The Oliver + Batlle service

A subscription model tailored to your needs

Stop worrying about optimising your dosing equipment. Our 3D nozzle service offers you a convenient, efficient printing solution with no long-term commitment, tailored to your needs.

How does it work?

  1. Ad-hoc study and design: Unlike purchasing a product, we begin with a preliminary study of your products and packaging lines for CAD development and functional prototyping of your custom nozzle.
  2. Scheduled production and delivery: Once the design has been validated, scheduled deliveries of the custom nozzles are established, ensuring that you receive the components just when you need them.
  3. Total flexibility: You can change, interrupt or cancel the service at any time. If your production varies, we offer an annual supply contract (min. 6 units) with adjusted prices and the possibility of an express service with guaranteed fast delivery (24 hours in Europe and 72 hours in the rest of the world).

Prices and contact

The prices of our service are determined based on your customisation needs and the volume of your supply plan.

  • Request a Personalised Quote: To discover the potential savings and prices of additive nozzles or the design service for a new nozzle, contact our sales team.

Optimizing production in the construction sector requires technology capable of handling complex materials. In this article, we analyse how Oliver + Batlle‘s advanced engineering solved the packaging challenges of Saint-Gobain Weber UK, the undisputed leader in industrial mortars and cutting-edge solutions in the United Kingdom.

Brief description of the company

Saint-Gobain Weber Ltd is a multinational subsidiary of the prestigious French group Saint-Gobain. The company stands out for its specialization in solutions for the construction and renovation of buildings, providing everything from industrial mortars and ceramic adhesives to advanced thermal insulation systems for facades and floors. Its commitment to quality has positioned it as a benchmark in new construction and restoration projects.

The challenge: Processing high-viscosity and abrasive products

The project focused on a highly complex technical challenge: the processing and packaging of wet plaster for plasterboard (stucco products).

This technical material has physical properties that make it difficult to handle:

  • Specific density:25–1.35 kg/dm³.
  • High viscosity: Between 500 and 3000 poises.
  • Abrasive nature: Requires superior mechanical robustness to ensure constant flow and accurate dosing without damaging the equipment.

Objective of the “Turnkey” project

The main challenge was to implement a turnkey production line capable of automating a previously manual process, while complying with Saint-Gobain Weber’s demanding standards:

  • High Performance: Achieve a stable rate of 10 containers of 20 kg (15L) per minute.
  • Maximum Gravimetric Accuracy: Maintain a variability of less than ±100g per container to drastically reduce raw material waste.
  • Process Integration: Intelligent connection via a handshake system with two existing 3,000L dispersers in the plant.
  • Innovation in dosing: Design of ad-hoc nozzles to optimize product distribution, avoiding stains in the closure area and ensuring a clean finish.

The Oliver + Batlle Solution: High-strength engineering

At Oliver+Batlle, we implement a comprehensive solution that complies with IP-54 protection standards and is manufactured with AISI-316 stainless steel in all contact areas to combat abrasion.

A) Feeding and Process Integration

  • Progressive Cavity Pumping Units: Two 15 kW helical pumping units with NBR stators and chrome-plated AlSi-316L stainless steel rotors, specifically designed for handling abrasive products.
  • Optimized Distribution: Complete installation of pipes and valves for efficient flow from the production area to the packaging area.

B) Automated Packaging Line

  • Pailmanager V-Flex Denester: Automatic system with capacity for stacks up to 400 mm in height. It enables fully automated format changeover managed from the HMI, with memory for up to 100 recipes, and incorporates photoelectric safety barriers to ensure operational protection.
  • OB-130-T Gravimetric filling unit: Dual-head system based on the “2-in-1” concept, optimizing the filling cycle without compromising accuracy.
  • Mettler Toledo Technology: Use of IND570 weighing terminals, ensuring metrological-grade accuracy and reliability in each dosing cycle.
  • Peripheral Systems and Traceability: Includes DT-350-S lids dispenser with lid presence detector, lid closing station CR-130 for flat press-on lids with manual adjustment, and a checkweigher with automatic rejection for out-of-tolerance containers.
  • Comprehensive Service: Full project scope, from P&ID and layout design to technical training of plant personnel.

Results

Thanks to the engineering solution implemented by Oliver + Batlle Saint-Gobain Weber UK has completely transformed the operational capacity of its plant in Flitwick.

The automated line continuously manages destacking, filling, and closing operations, allowing a sustained production rate of 10 units per minute to be achieved. The use of the OB-130-T Gravimetric Filling Machine allows for interleaved filling, optimizing cycle time without compromising the precision required for high-viscosity products.

This technical approach maximizes the profitability and efficiency of the process:

  • Cost optimization: The high precision of ±100g, together with the automatic rejection system, eliminates costly overfilling and raw material waste, accelerating return on investment.
  • Operational agility: Downtime between batches is drastically reduced thanks to the automated format changeover managed via the HMI of the Pailmanager V-Flex.
  • Reliability and durability: The use of AISI-316 stainless steel and the robustness of the helical pump units ensure a long service life for components despite the abrasive nature of technical putty.

As a result, the overall performance of the installation is improved, ensuring the high efficiency and quality standards required by the Saint-Gobain group for its construction solutions.

Conclusion

The success achieved in this project demonstrates that high viscosity and the abrasive nature of technical materials  are not obstacles when the right technology is in place. The satisfaction of Saint-Gobain Weber UK, reflected in the words of Toni Wallis—who highlights that Oliver + Batlle‘s solution has enabled them to meet their highest efficiency standards—is the best endorsement of our engineering expertise.

If your plant is also facing challenges in the packaging of technical products, we invite you to discover how we can help transform your operations.


You can see the complete process in the following video available on our YouTube channel.