Introduction
A leading company in the industrial paints and coatings sector undertook a strategic project aimed at optimising its manufacturing and filling processes for solvent-based industrial paint. The objective was to implement a highly automated installation capable of handling complex formulations, multiple raw materials, and different batch sizes, whilst maintaining the highest standards of quality, safety, traceability, and environmental responsibility.
Oliver + Batlle participated in the development and implementation of the technological solutions required to meet these objectives, contributing its expertise in dosing systems, manufacturing processes, and process control for the paints industry.
Product to be processed
The project focused on the manufacturing and filling of solvent-based industrial paint, intended for the protection and decoration of surfaces, with high requirements in terms of homogeneity, repeatability, and final product performance.
Project objectives
The company sought a solution that would enable the manufacturing and filling of a wide variety of products, in different batch sizes, through fully automated and highly controlled processes.
The main technical challenges of the project were:
- Management of a large number of raw materials, with more than 60 different products, including solids and liquids, many of them transferred via piping.
- Ensuring the required quality for each formulation, regardless of its complexity.
- Guaranteeing full traceability of raw materials and process operations.
- Maintaining optimal safety and hygiene conditions, with a design focused on zero pollution, for both solids and liquids, despite working with solvent-based products.
- Fully automating the production process through recipe execution from the control system.
Solutions provided by Oliver + Batlle
Oliver + Batlle developed and integrated a set of process and automation solutions, specifically designed to meet the requirements of a leading manufacturer in the sector.
Solid dosing and conveying
For the handling of solid raw materials, the following solutions were implemented:
- Installation of four 6 m³ mini-silos for powder raw materials, with automatic transfer through a pneumatic conveying system running throughout the plant to the different consumption points.
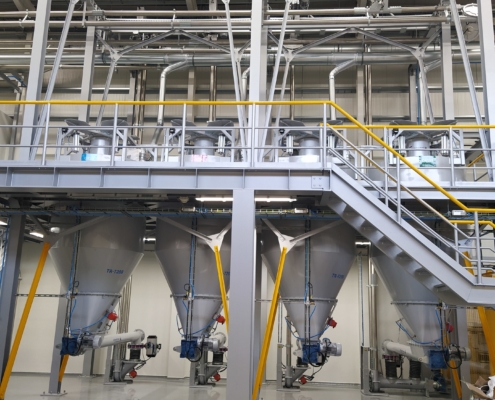
- Dosing station for solids not stored in silos, supplied from bags or big-bags, with direct pneumatic conveying to the dispersers used for large-batch production.
- Mechanical conveying system with a capacity of up to 6 t/h, designed to automatically feed and dose solids to four dispersers located on the process platform.
Liquid dosing
The solution incorporates an automatic liquid dosing system, integrated into recipe management, enabling precise dosing of:
- Major raw materials, such as resins and solvents.
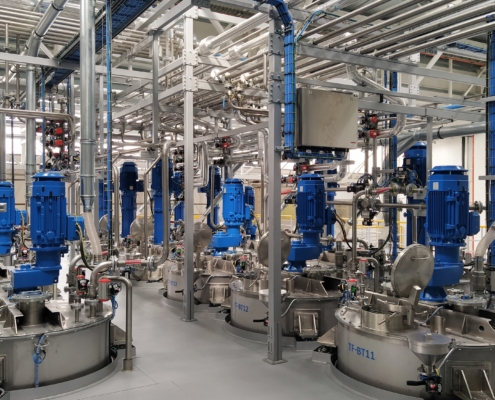
- A large number of additives, managed according to defined formulations.
Manufacturing and finishing processes
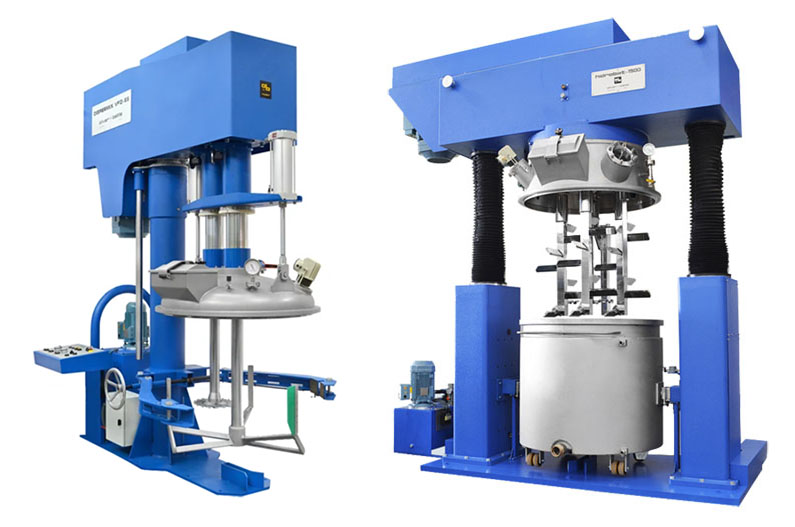
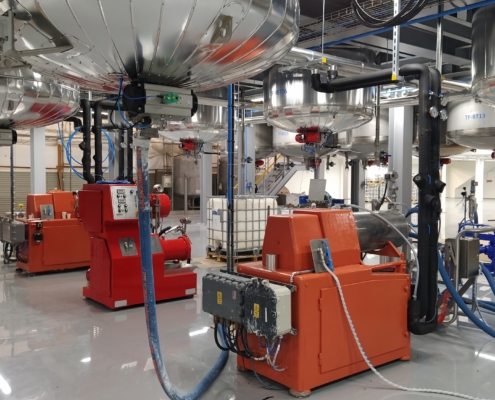
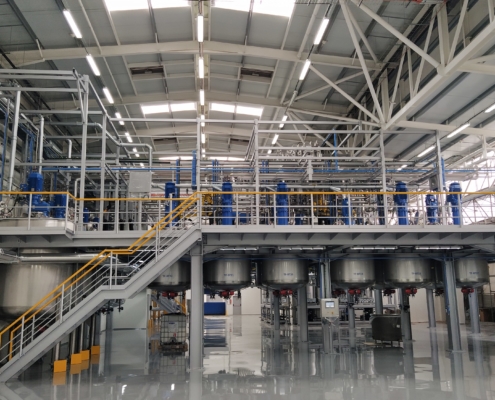
The Mill Base is manufactured in single-shaft and three-shaft dispersers, from which the product is transferred to intermediate tanks through milling processes.
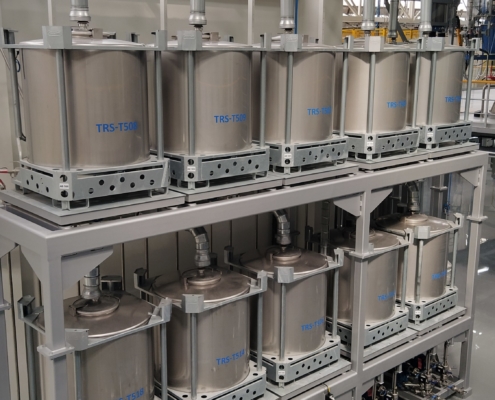
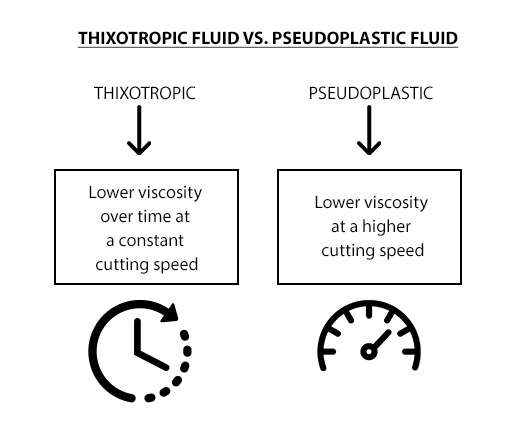
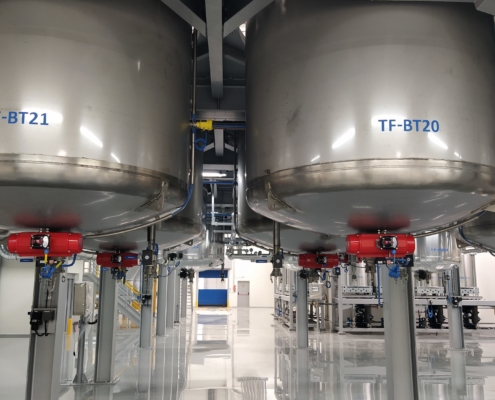
The milled products are then transferred to finishing tanks of different capacities, equipped with mixing systems specifically designed according to the type of product and its rheological requirements.
Small-batch production
The solution combines large-batch manufacturing with short-run production through:
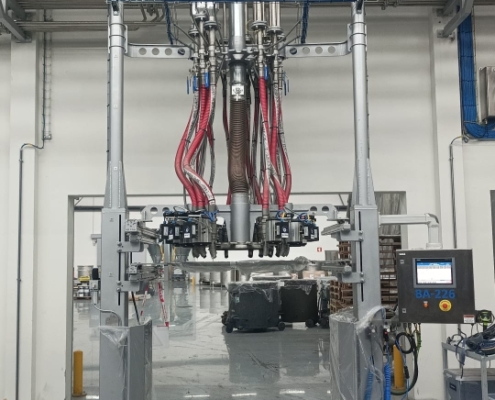
- Four automatic dosing stations, capable of managing multiple different products per recipe.
- Dosing heads with horizontal movement, facilitating manual dosing from drums.
- A set of 19 process units, including dispersers, mixers, and milling systems, dedicated to small-batch production.
Automation and traceability
The entire installation is governed by a fully automatic control system, with recipe management and communication with the customer’s ERP, enabling centralised control of all manufacturing operations.
In addition, a barcode creation and reading system was integrated for manually added products, ensuring complete traceability of raw materials and the production process.
Results
The implemented solutions allow this leading company to operate a highly flexible, safe, and efficient industrial paint manufacturing and filling system, capable of handling a wide variety of formulations and batch sizes.
Key benefits achieved:
- High production flexibility, adapted to a broad product portfolio.
- Full automation, ensuring accuracy, repeatability, and process control.
- Maximum safety and hygiene, with a plant designed to operate under zero-pollution conditions.
- Strong environmental commitment, even in processes involving solvent-based products.
Our technical team can help you define the most suitable solution for your process