Challenge: Increase production capacity without expanding facilities, working with variable batches of varnishes and water-based and solvent-based paints.

Solution: Polimix DPS-5000-TRC ATEX disperser.

Result: Significant increase in production capacity, greater operational flexibility, and reduction in manual operator intervention.


1. IRURENA GROUP

IRURENA Group is a family-owned industrial company founded in 1969, specialized in the manufacture of varnishes and paints for industrial applications, mainly on wood, in both water-based and solvent-based formulations.

2. Products and Manufacturing Challenges

  • Water-based paints for industrial applications on wood
  • Solvent-based paints with ATEX requirementsTechnical complexity: The variability of formulations and production volumes required a dispersion system capable of adapting to different products while maintaining process quality and production efficiency.
  • Industrial varnishes for high-quality professional finishes on wood

Technical complexity: The variability of formulations and production volumes required a dispersion system capable of adapting to different products while maintaining process quality and production efficiency.

3. Project Objectives

Main objective: Increase the production capacity of the existing plant by incorporating new dispersion equipment capable of working with both small and large batches, without the need to expand facilities or modify the manufacturing platform.

Challenge Description
Space Integration of equipment in a reduced space, within an already operational production facility.
Coordination Technical coordination with different project contractors, ensuring proper integration with auxiliary systems for liquid and solid feeding, dust and vapor extraction, cleaning solvents, complying with ATEX requirements.
Installation Execution of complex maneuvers, conditioned by equipment dimensions and plant access limitations.

Critical requirement: The entire project had to guarantee safe, reliable operation oriented toward optimizing daily operations.

4. Implemented Solution


Polimix DPS-5000-TRC ATEX Equipment

Oliver + Batlle designed and manufactured a high-power disperser specifically configured for the client’s production needs, ensuring maximum efficiency and operational safety.

Main Technical Features

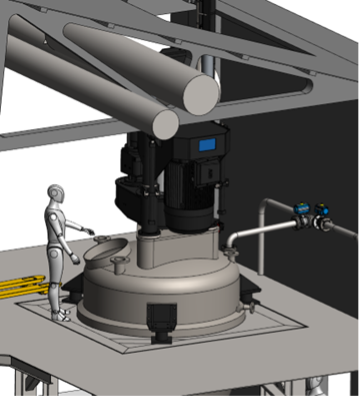
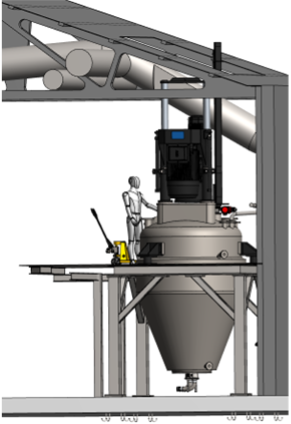
  •   Truncated-conical design: Allows efficient work with both small and large product volumes
  •   Disperser shaft raising and lowering system: Provides flexibility and control during the manufacturing process
  •   Half-pipe cooling jacket: Ensures thermal stability of the product during dispersion
  •   Automatic cleaning system: Using mobile lances, with integrated process control
  •   Complete control of the equipment: HMI touchscreen in classified zone, while  PLC and electrical cabinet are located in safe area, fully compliant with ATEX requirements.

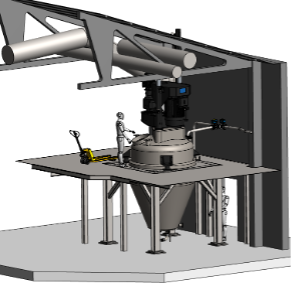
The equipment was installed on a carbon steel support structure with primer coating, designed at the same height as the existing production platform. Oliver + Batlle provided the loads transmitted to the floor so that the client could execute the corresponding foundations, as well as the anchor plates on which the structure and the equipment rest. The position of the liquid and powder loading connections and the vapour/dust extraction points was also defined.

A specialized technician from Oliver + Batlle coordinated the positioning operations, final assembly, and commissioning of the equipment, ensuring its proper integration into the plant.

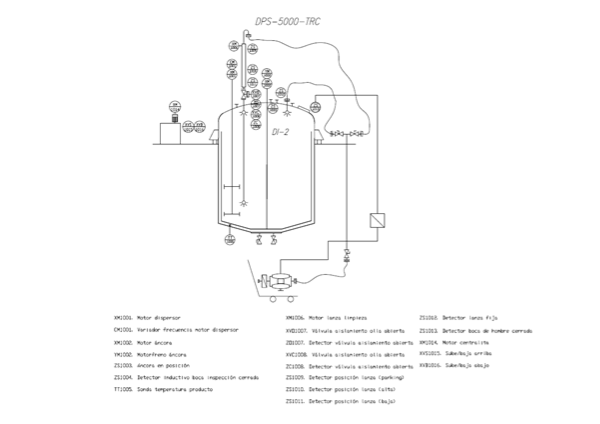
Process diagram of supplied equipment:
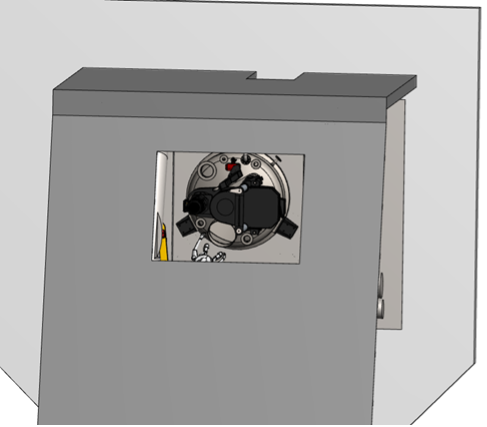
3D views of the equipment on its structure, integrated in the existing factory:
5. Results

  •  Significant increase in the production capacity of the existing plant without the need to expand facilities
  • Maximum operational flexibility: production of large and small batches of a wide variety of products using a single disperser
  • Improved efficiency of the production process through integrated automatic control
  • Reduced operator intervention: manual and automatic operation, and integrated cleaning system

6. Conclusion 

This project demonstrates how a customized engineering solution, properly integrated into an existing installation, optimizes production and prepares the plant for future growth.

The combination of specialized technical design, ATEX regulatory compliance, integration within reduced space, and process automation has enabled IRURENA GROUP to strengthen its competitive position in the industrial coatings market.
Company overview

Duracolor Coatings, S.L.U. is a family-owned company dedicated to the manufacture of a wide range of coatings, both water-based and solvent-based, including emulsion paints, exterior coatings, primers, enamels, varnishes and wood finishes.

With a strong industrial background dating back to the 1980s, Duracolor markets its products both in the domestic market and internationally, particularly in South America and Africa, through specialised distributors. Throughout its history, the company has continuously invested in improving its production processes to meet growing demands for quality, flexibility and capacity.

Product to be processed

Water-based emulsion paints and exterior coatings.

Project objective

Duracolor Coatings identified the need to increase the production capacity of its water-based product range (emulsion paints and exterior coatings), under a number of key technical constraints:

  • Installation of the new equipment in a limited space, adjacent to the existing dispersion area, originally supplied by Oliver + Batlle in the late 1990s.
  • Close coordination with the different contractors involved in the project, including:
    • Manufacturer of the working platform.
    • Installers of solid and liquid feeding systems.
    • Dust and vapour extraction systems integrated with the Oliver + Batlle equipment.

The objective was to integrate the new manufacturing units while maintaining production continuity, optimising the use of available space and ensuring appropriate safety, ergonomics and operational efficiency.

Oliver + Batlle solution

Oliver + Batlle designed and supplied a solution fully adapted to the specific requirements of Duracolor’s plant, including the following equipment:

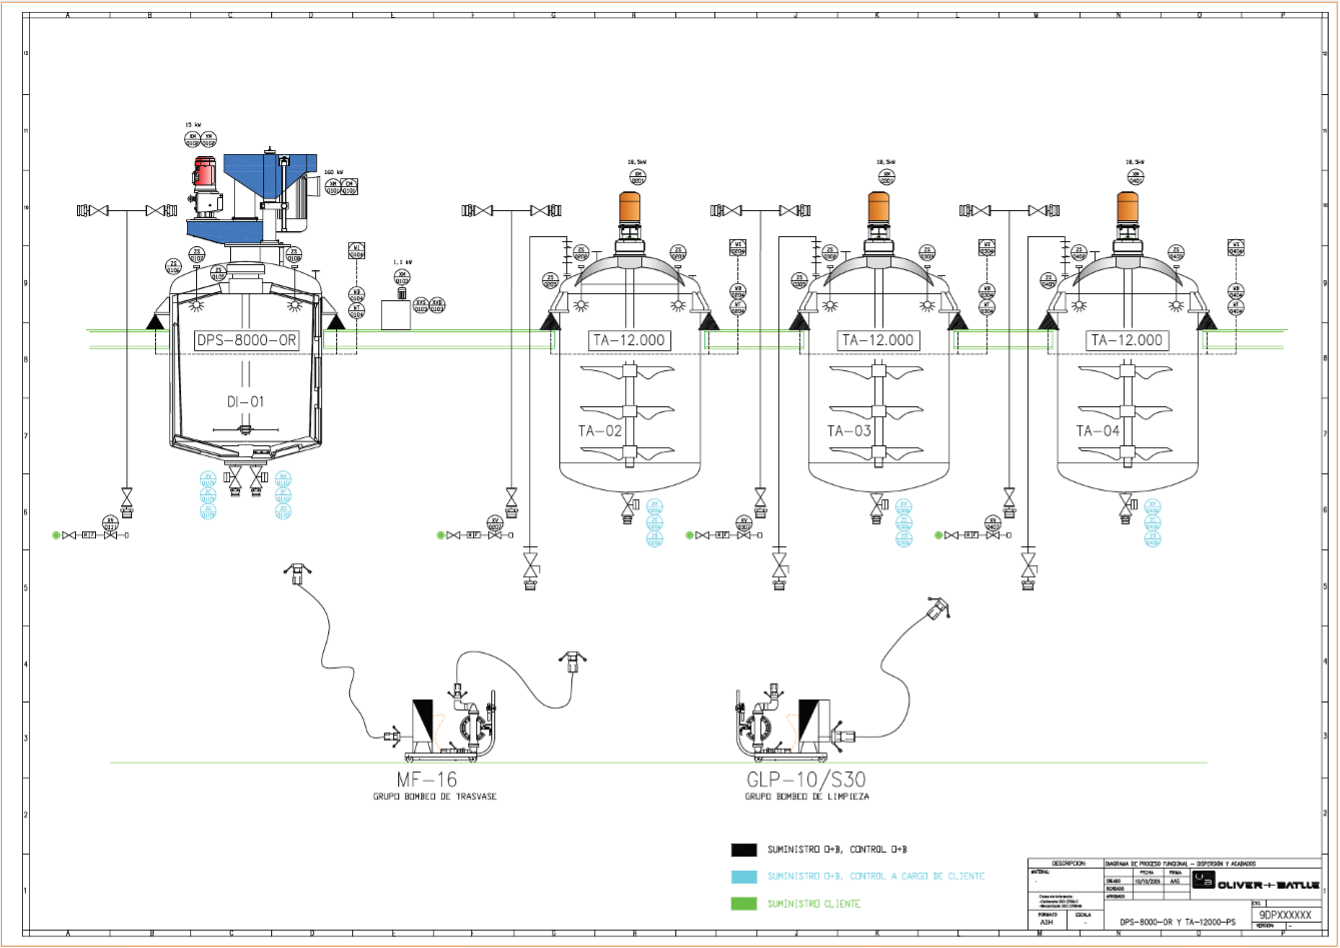
  • Polimix DPS-8000-OR, standard power, equipped with:
    • Integrated weighing system.
    • Automatic discharge valves.
    • Fixed cleaning lances.
    • Cleaning pump unit GLP-10/S-30.

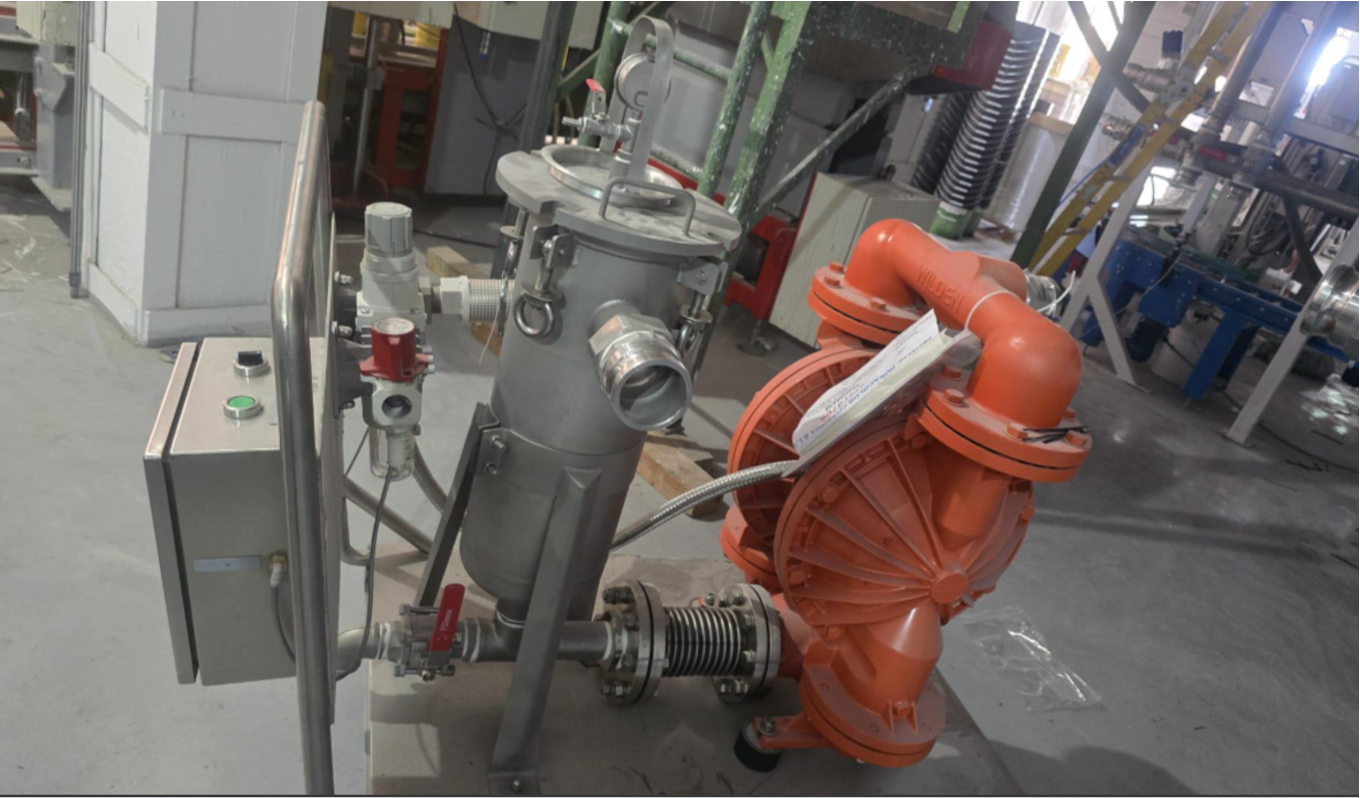
  • MF-16 pumping unit with filter, for transferring the paste produced in the Polimix to the finishing tanks.
  • Three TA-12000-PS finishing tanks, each equipped with:
    • Weighing system.
    • Automatic discharge valve.
    • Fixed cleaning lances.

Dynamic load calculations for the existing structure were provided, and the final location of the Polimix and the finishing tanks within the available space was jointly agreed, arranging them in a triangular (staggered) layout in order to optimise access, traffic flow and operational accessibility.

In addition, the position and sizing of the following were also jointly defined:

  • Liquid and powder feeding connections for the Polimix unit.
  • Dust and vapour extraction systems for the Polimix unit.
  • Liquid feeding connections and vapour extraction for the Finishing Tanks.

Process flow diagram of the supplied equipment

Results

As a result of the implemented solution, Duracolor Coatings has significantly increased the production capacity of its existing plant.

  • The Polimix is used for the paste preparation stage, incorporating water, powders and additives.
  • The paste is then transferred to the Finishing Tanks, where the formulation is completed by adding emulsions, water and final additives.

This production concept allows overlapping operations: while a batch is being finalised in a finishing tank, a new paste can be prepared in the Polimix. As a result, manufacturing times are optimised, overall plant productivity is improved, and the quality and homogeneity of the final product are ensured.


Introduction

A leading company in the industrial paints and coatings sector undertook a strategic project aimed at optimising its manufacturing and filling processes for solvent-based industrial paint. The objective was to implement a highly automated installation capable of handling complex formulations, multiple raw materials, and different batch sizes, whilst maintaining the highest standards of quality, safety, traceability, and environmental responsibility.

Oliver + Batlle participated in the development and implementation of the technological solutions required to meet these objectives, contributing its expertise in dosing systems, manufacturing processes, and process control for the paints industry.

Product to be processed

The project focused on the manufacturing and filling of solvent-based industrial paint, intended for the protection and decoration of surfaces, with high requirements in terms of homogeneity, repeatability, and final product performance.

Project objectives

The company sought a solution that would enable the manufacturing and filling of a wide variety of products, in different batch sizes, through fully automated and highly controlled processes.

The main technical challenges of the project were:

  • Management of a large number of raw materials, with more than 60 different products, including solids and liquids, many of them transferred via piping.
  • Ensuring the required quality for each formulation, regardless of its complexity.
  • Guaranteeing full traceability of raw materials and process operations.
  • Maintaining optimal safety and hygiene conditions, with a design focused on zero pollution, for both solids and liquids, despite working with solvent-based products.
  • Fully automating the production process through recipe execution from the control system.

Solutions provided by Oliver + Batlle

Oliver + Batlle developed and integrated a set of process and automation solutions, specifically designed to meet the requirements of a leading manufacturer in the sector.

Solid dosing and conveying

For the handling of solid raw materials, the following solutions were implemented:

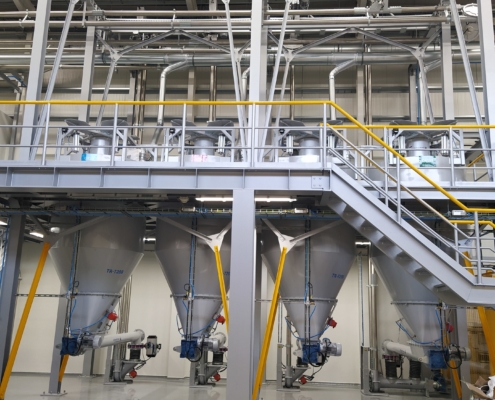
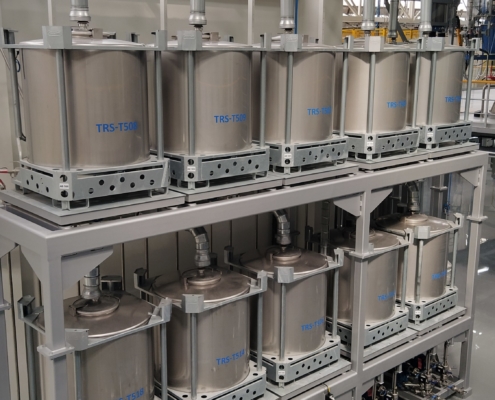
  • Installation of four 6 m³ mini-silos for powder raw materials, with automatic transfer through a pneumatic conveying system running throughout the plant to the different consumption points.
  • Dosing station for solids not stored in silos, supplied from bags or big-bags, with direct pneumatic conveying to the dispersers used for large-batch production.
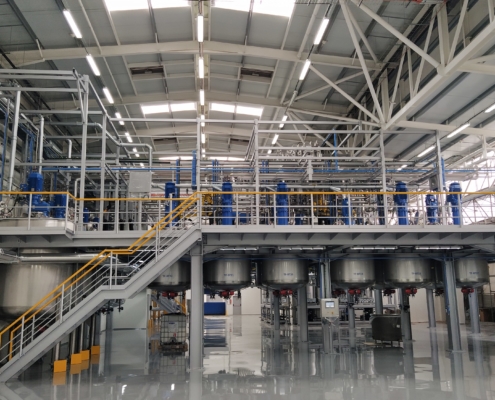
  • Mechanical conveying system with a capacity of up to 6 t/h, designed to automatically feed and dose solids to four dispersers located on the process platform.

Liquid dosing

The solution incorporates an automatic liquid dosing system, integrated into recipe management, enabling precise dosing of:

  • Major raw materials, such as resins and solvents.
  • A large number of additives, managed according to defined formulations.

Manufacturing and finishing processes

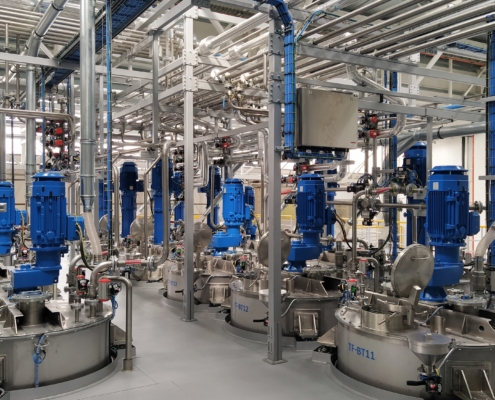
The Mill Base is manufactured in single-shaft and three-shaft dispersers, from which the product is transferred to intermediate tanks through milling processes.

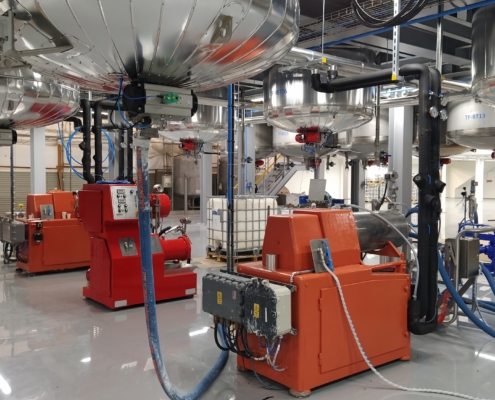
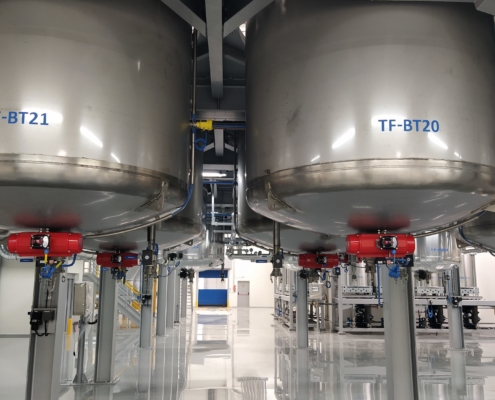
The milled products are then transferred to finishing tanks of different capacities, equipped with mixing systems specifically designed according to the type of product and its rheological requirements.

Small-batch production

The solution combines large-batch manufacturing with short-run production through:

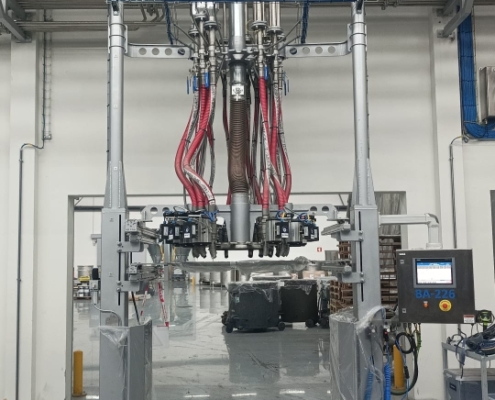
  • Four automatic dosing stations, capable of managing multiple different products per recipe.
  • Dosing heads with horizontal movement, facilitating manual dosing from drums.
  • A set of 19 process units, including dispersers, mixers, and milling systems, dedicated to small-batch production.

Automation and traceability

The entire installation is governed by a fully automatic control system, with recipe management and communication with the customer’s ERP, enabling centralised control of all manufacturing operations.

In addition, a barcode creation and reading system was integrated for manually added products, ensuring complete traceability of raw materials and the production process.

Results

The implemented solutions allow this leading company to operate a highly flexible, safe, and efficient industrial paint manufacturing and filling system, capable of handling a wide variety of formulations and batch sizes.

Key benefits achieved:

  • High production flexibility, adapted to a broad product portfolio.
  • Full automation, ensuring accuracy, repeatability, and process control.
  • Maximum safety and hygiene, with a plant designed to operate under zero-pollution conditions.
  • Strong environmental commitment, even in processes involving solvent-based products.

Our technical team can help you define the most suitable solution for your process


1. Company Overview

Founded in 1961, Pinturas Montó began its activity in Valencia producing vegetable glues and traditional tempera paints. Over the years, it evolved into the manufacture of decorative plastic paints, becoming a benchmark brand in the sector.

Since 1996, the company has operated from its 46,000 m² facility in Marines (Valencia), equipped with advanced manufacturing and quality-control technology. Montó maintains a firm commitment to innovation, sustainability and international expansion, achieving a production capacity of over 200,000 L per day with a consolidated presence in multiple countries.


2. Product to be processed

Pinturas Montó offers a complete product range for the decorative and professional markets, including:

  • Interior plastic paints (matt, mid-sheen and satin).
  • Exterior façade coatings (siloxanic, monocapa, SATE systems).
  • Water-based enamels for multiple substrates.
  • Fillers, primers and surface-preparation products.
  • Tinting systems with bases, colourants and proprietary software.
  • Technical coatings: damp-proof, intumescent, wood protection and sports-floor coatings.


3. Project objective

Pinturas Montó identified the need to increase its production capacity for manufacturing large batches of white water-based paint, both for its own brand and for third parties. The main objective was to achieve a continuous, stable and highly efficient production flow, optimising time, resources and operating costs.

Although the company already had process equipment, the rise in demand required a fully automated line capable of integrating:

  • Manufacturing
  • Filling
  • Palletising

The installation also had to handle two different container ranges simultaneously:

  • Small formats (up to 5 L)
  • Large formats (up to 20 L)

This led to the design of a dual-line, high-output filling system, ensuring the performance, accuracy and efficiency required by Pinturas Montó.


4. Oliver + Batlle solution

Oliver + Batlle provided a comprehensive solution combining continuous production, automated filling and in-line quality control.

Production

A Dispermix VF-400-E was installed together with two 20,000-L tanks positioned on the customer’s existing platform.

This setup allows:

  • Manufacturing a new batch while the previous one is being filled
  • Eliminating downtime
  • Maintaining a constant feed to the filling lines

Automatic filling – dual line

Two automatic lines with a common structure were implemented:

Filling line for large-containers (up to 20 L)

Featuring:

  • Automatic pail denester PAILMANAGER
  • Automatic labelling machine
  • Flash-25-T , volumetric filling machine including:
    • Two dosing heads
    • Two independent hoppers
    • Lid dispenser and closing unit
    • Checkweigher with automatic correction
    • Rejecting system

The checkweigher communicates with both dosing heads, automatically adjusting volumes according to variations in the paint’s rheological behaviour.

Filling line for small-containers (up to 5 L)

Featuring:

  • Semi-automatic feeding table SQ
  • Automatic labelling machine
  • Volumetric filling unit Flash-55-S, equipped with a single dosing head and offering similar features to the Flash-25-T , optimised for smaller formats.


5. Results

Continuous production: While one 20,000-L tank feeds the filling lines, the next batch is manufactured in the second tank, ensuring constant flow and eliminating downtime.

Reduced cleaning time: As the line works exclusively with white paint, cleaning is required only once a week, significantly reducing downtime and associated costs.

Increased productivity: Full automation and the ability to handle up to 29 different formats enable Montó to meet both internal demand and third-party production with greater flexibility and speed.


Introduction

If your manufacturing process for paints, sealants, or putties involves a change in viscosity when stirred, you are working with thixotropy. But do you know how to measure and control this phenomenon to guarantee consistency in the container and ease of application?

Thixotropy is the fundamental rheological property by which some complex fluids drastically modify their viscosity, becoming more fluid, when a shear force (such as stirring) is applied to them. This phenomenon is key: the fluid has a high equilibrium viscosity at rest and “liquefies” during working.

Below, we will delve into the concept, explore the crucial difference with pseudoplastic fluids, and analyse how thixotropy determines the choice of the most efficient machinery in the manufacturing, finishing, and packaging phases of your products.

1. What Thixotropy is and Why it is Crucial in Viscosity

The technical concept of thixotropy involves the decrease in viscosity over time under a constant stress or shear rate, followed by a gradual recovery of the original viscosity (equilibrium viscosity) when that stress ceases.

Think of it this way: the paint in the pot is thick (high equilibrium viscosity), but when stirred or applied with a brush, it becomes fluid (low viscosity), allowing for application. Once on the wall, the shearing ceases and the product quickly recovers its initial viscosity, preventing sagging.

1.1. The Key Difference: Thixotropic vs. Pseudoplastic

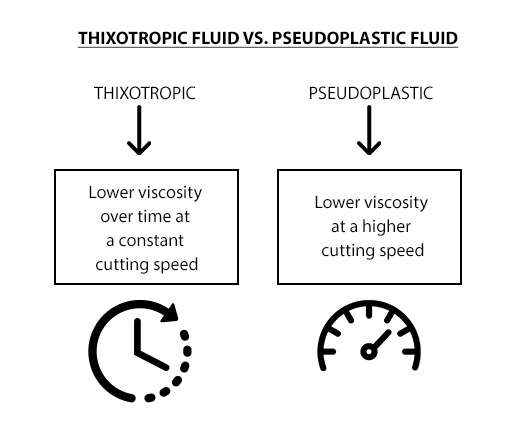
It is common for thixotropy to be confused with the behaviour of pseudoplastic fluids. Although both show a decrease in viscosity with shearing, the time difference is fundamental:

1.2. Rheopectic: The Opposite Behaviour (Anti-Thixotropy)

In contrast, fluids that exhibit the opposite behaviour to thixotropy, where constant stirring causes solidification or an increase in viscosity over time, are called rheopectic or anti-thixotropic. These products are significantly less common in the coatings industry.

thixotropy vs pseudoplastic

2. Thixotropy and Manufacturing: The Demand on Industrial Machinery

Thixotropy does not affect all formulations equally. Products such as varnishes, lacquers, and traditional synthetic and water-based paints are usually non-thixotropic. However, highly specialised products such as wood sealants, waterproofing paints, and repair putties are eminently thixotropic.

When selecting manufacturing machinery, it is imperative to know the level of thixotropy of the product. The stirring equipment must meet two key requirements to ensure homogeneity:

  1. Offer the adequate power to break the fluid’s initial thixotropy.
  2. Maintain a constant speed for the time necessary to reach the optimum working state.

2.1. Specific Equipment for High Thixotropy Products

The equipment from Oliver + Batlle is designed to manage these rheological challenges with high efficiency:

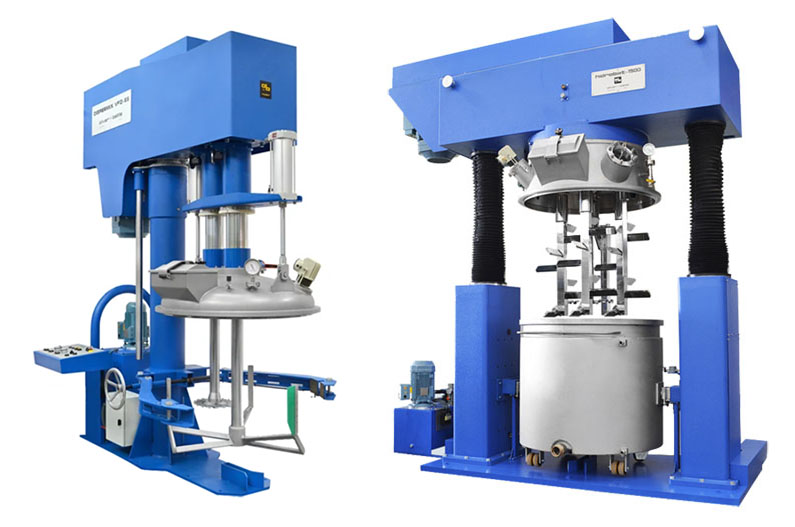
  • Dual Dispermix: Suitable for medium and high viscosity products that exhibit moderate thixotropy.
  • Hidrobat Planetary Mixer: The ideal solution for high viscosity and very thixotropic products (and also pseudoplastic ones), ensuring intensive and uniform working.

mezcladores productos tixotropicos

It is important to remember that, once manufactured and agitation has stopped, the product cools and increases its viscosity, acquiring the appropriate rest state for its final application.


3. The Thixotropic Packaging Challenge: Dosing and Pumping Solutions

The packaging of thixotropic products presents its own set of challenges, the main one being the difficulty of extracting the product from the container due to its high equilibrium viscosity.

3.1. Tank Emptying: Hydraulic Presses and Volumetric Equipment

To facilitate the emptying of portable tanks (which often reach 1,500 litres), high-force extraction equipment is required:

  • Hydraulic Press Systems (PH or PCH – TVH Press): The pressing pressure is capable of extracting medium and high thixotropic viscosity products that would otherwise be impossible to pump at rest.

Once out of the tank, the most precise measuring and dosing systems are volumetric type (such as the DVB 250), which can be easily automated with container conveying and closing systems.

3.2. Industrial Filling Machines: Gravimetric and Positive Displacement

In the Oliver + Batlle portfolio, we have specific solutions for different capacities:

  • Low Volume Filling Machines (E.g., Model EM 52): Designed for packaging highly thixotropic and high viscosity products in containers of up to 250 cc (common in offset inks or repair putties).
  • High Volume Filling Machines (E.g., DG 60 or OB 130): These gravimetric filling machines are fed by electric positive displacement screw pumps, as these better handle the high viscosity and nature of the fluid.

Process Note: To avoid suction problems in the pumps, it is vital that thixotropic products remain under agitation in the finishing tank during the packaging phase.

Conclusion: The Need for Rigorous Control

Thixotropy is a complex but essential property for the final quality of specialised coatings. Understanding the difference with pseudoplastic fluids and applying the correct stirring and extraction regime not only guarantees a homogenous product but also optimises the packaging process.

Do not risk the quality of your formulation. If you want to guarantee that your thixotropic products are manufactured and packaged with maximum efficiency and according to specifications, you need the right machinery.

Act Now! We invite you to contact the Oliver + Batlle specialists directly to request technical advice and discover which equipment (stirrers, presses, or filling machines) best suits the exact profile of your products.