Development and Scale-Up of Paraffin Emulsion via Phase Inversion
1. Brief company description
Oliver + Batlle works in collaboration with a company specializing in the production of emulsifiers (paraffin emulsions), moisturizing agents, and solutions formulated with fats, waxes, and oils for the cosmetics, pharmaceutical, and home care sectors. Its focus is on sustainable innovation and the development of customized products designed to meet the specific needs of each industrial client.
2. Product to be processed
Paraffin-in-water emulsion, produced through a phase inversion process (W/O -> O/W), with 50% resin content.
The process begins with melting and mixing high-viscosity solids and ends with a fluid emulsion after the critical inversion phase. This variation in viscosity requires a custom-designed anchor agitator and heating at temperatures above 150°C.
3. Objective
Starting from a consolidated laboratory process for manufacturing this complex emulsion, the need was to scale it up to an industrial level.
The goal was to achieve a stable dispersion of 50% resin via phase inversion, while avoiding foam formation.
The main technical challenge appeared in the pre-inversion stage, where the product is especially viscous and difficult to mix Additionally, temperature control and water feed rate were identified as critical factors for final product stability.
4. O+B SOLUTION
OLIVER + BATLLE proposed a co-development strategy with the customer, using its in-house pilot plant to validate the mixing system design and tailor the equipment to the product’s characteristics.
Phase 1 – Pilot trials
Three pilot trials were carried out on a 150 L Polimix system, configured with a custom anchor (slow shaft) and a high-speed disperser (coaxial configuration).
The trials used thermal oil at over 150 °C to reach the required process temperature.
The goal was to validate the mixing capacity for achieving stable phase inversion.
Results:
- Phase inversion was successfully achieved.
- Some stability issues were detected in the batches compared to the target sample, attributed to process parameters (temperature and water flow) rather than the mixing system.
- Equipment performance was excellent in terms of viscosity handling and behavior under critical conditions.
Phase 2 – Final solution
After confirming the technical feasibility, the customer acquired:
- 1 pilot unit VF-11 Special, with custom-designed anchor
- 1 thermal oil heater for the VF-11
- 1 production unit DPS-6000-OR Special, also equipped with the same custom agitator system and prepared for steam heating
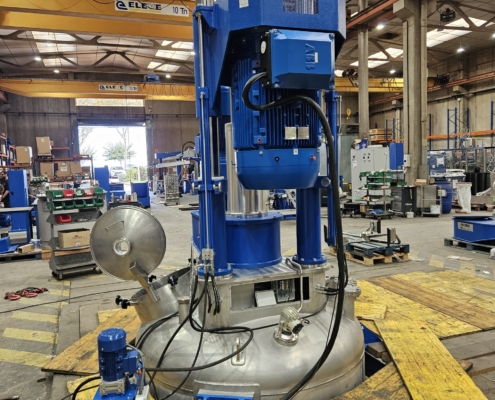
During the manufacturing phase, the customer maintained access to the O+B pilot lab to continue developing the product, ensuring a smooth transition from pilot to industrial scale.
5. Results
- Validation of the phase inversion process in a simulated industrial environment
- Custom anchor design tailored to the emulsion’s mixing needs
- Successful scale-up from laboratory to industrial equipment
- Reduced technical risk thanks to joint development using O+B’s lab
- Equipment currently installed and operational at the customer’s plant.