HIGH-CAPACITY REACTOR FOR THE PRODUCTION OF SPECIAL RESINS
1. BRIEF DESCRIPTION OF THE CLIENT
An international textile-sector company with a highly integrated and sustainable insfrastructure, dedicated to the manufacture of high added-value products from recycled fibres and organic raw materials. With benchmark production capacity in its market, its industrial strategy prioritises efficiency, innovation, and the independence of key processes.
2. PRODUCT TO BE PROCESSED
Special resin used as a base component in formulations for technical textile applications.
3. OBJECTIVE
The client aimed to establish its own in-house production unit for this strategic resin, which had previously been purchased from external suppliers, in order to strengthen industrial autonomy and optimise production costs.
4. OLIVER + BATLLE SOLUTION
To address this challenge, Oliver + Batlle designed and implemented:
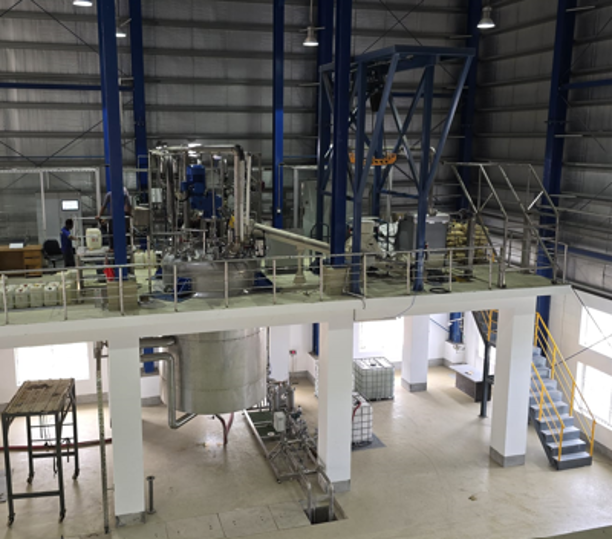
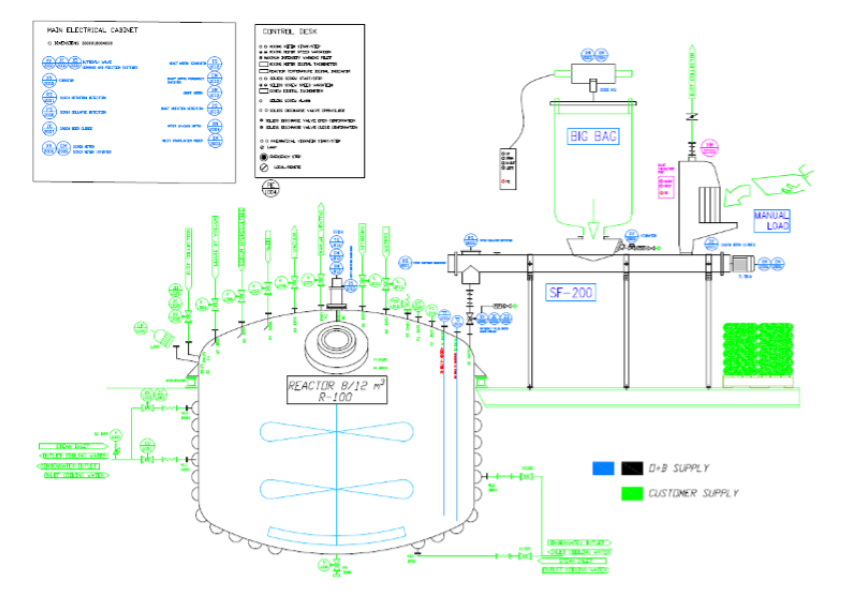
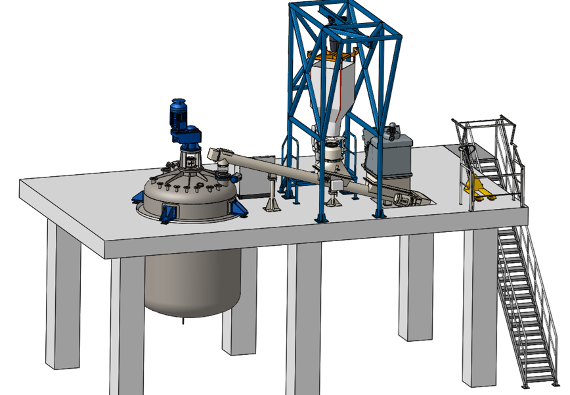
– 12,000-litre reactor for resin synthesis through monomer reaction, featuring:
- Three-section half-coil for precise thermal control using steam and cooling water
- Agitator shaft with two INTERMIG-type blades, Ø1850?mm
- Semi-anchor Ø1700?mm
- Construction material: AISI 316L stainless steel
- Reactor working temperature: up to 150°C
- Reactor working pressure: absolute vacuum to 3 bar g
- Half-coil working temperature: up to 200°C
- Half-coil working pressure: up to 10 bar g
- 37 kW agitator motor with frequency converter
– Solids loading system using a screw conveyor, with sack and Big Bag unloading stations
– Complete process control system, including supervision of installation and commissioning on site
5. RESULTS
The project met the client’s needs with a robust, reliable and hygienic solution, ensuring consistent performance fully aligned with the highest quality standards.